




Email: sales3@zhefanjewelry.com
PVD Coating vs Electroplating for Jewelry: A B2B Buying Guide for 925 Silver and Brass
Compare PVD coating and electroplating for 925 silver and brass jewelry, including durability, gold claims, testing, cost, and sourcing decisions.
- Executive Summary for Jewelry Buyers
- What Is PVD Coating?
- Does Gold-Colored PVD Contain Real Gold?
- What Is Traditional Electroplating?
- PVD vs Electroplating: Technical and Commercial Comparison
- Which Process Is More Durable?
- Are PVD and Electroplated Jewelry Waterproof?
- PVD and Electroplating on Brass and 925 Sterling Silver
- Brass Jewelry
- 925 Sterling Silver Jewelry
- Gold-Plated and Gold-Vermeil Requirements in the United States
- EU REACH Requirements for Jewelry
- Testing and Acceptance Criteria for B2B Orders
- XRF Coating-Thickness Measurement
- Adhesion Testing
- Salt-Spray Testing
- How Buyers Should Interpret Test Results
- Cost, MOQ, and Lead-Time Considerations
- From Quotation to Bulk Production
- How to Evaluate a PVD or Electroplating Manufacturer
- Final B2B Recommendation
- Request a Design-Specific Coating Recommendation
- FAQ
Choosing between PVD coating and traditional electroplating is not simply a matter of selecting the newer, harder, or more expensive process. For jewelry brands, wholesalers, and product developers, the correct surface treatment depends on the complete product system, including the base alloy, polishing quality, intermediate layers, final coating, product geometry, soldering, stone setting, target market, and expected wearing conditions.
PVD can provide a hard decorative surface, improved abrasion performance, and engineered colors such as black, gunmetal, and gold-like yellow. Electroplating remains essential when a product requires genuine gold, silver, rhodium, or palladium; a specified precious-metal thickness; surface leveling; or more reliable coverage across recessed areas.
For selected brass and 925 sterling silver designs, electroplating and PVD should not always be treated as competing technologies. A carefully designed system may use electroplated layers to create a smooth and corrosion-resistant foundation, followed by a PVD film that provides the final color and wear characteristics.
The right sourcing question is therefore not simply, “Is PVD better than electroplating?” It is:
“Which coating structure is technically, legally, and commercially appropriate for this specific jewelry design?”
Executive Summary for Jewelry Buyers
|
Product Requirement |
Usually the More Appropriate Direction |
Main Buyer Check |
|
Genuine 14K or 18K gold-plated jewelry |
Verified genuine-gold electroplating or another qualified gold-deposition process |
Confirm gold composition, karat, thickness, coverage and measurement method |
|
Gold vermeil jewelry |
Sterling silver base with a qualifying genuine-gold or gold-alloy coating |
Verify base material, gold fineness, equivalent fine-gold thickness and market requirements |
|
Black, gunmetal or engineered decorative colors |
PVD coating |
Confirm coating chemistry, approved color standard and substrate compatibility |
|
Brass jewelry requiring improved barrier and wear performance |
Electroplated leveling and barrier layers, with PVD considered as a top layer |
Review the complete coating system rather than only the visible layer |
|
Deep recesses and complex internal surfaces |
Electroplating is generally more suitable for broad conductive coverage |
Validate appearance and thickness in hidden and low-current-density areas |
|
Adjustable rings, flexible chains and moving parts |
Design-specific sample and flex testing |
Confirm bending, deformation and repeated-movement performance |
|
EU skin-contact jewelry |
Either process may be used, but the finished article must meet applicable restrictions |
Evaluate nickel release, lead, cadmium and other restricted substances |
PVD is not automatically waterproof, hypoallergenic, or permanently fade-resistant. Electroplating is not automatically outdated or lower quality. The performance of either process depends on the design and control of the complete coating structure.
What Is PVD Coating?
PVD stands for Physical Vapor Deposition. It is a family of vacuum-deposition processes in which a coating material is released from a solid source and deposited as a thin film on the product surface. Common methods include magnetron sputtering, cathodic arc deposition, and vacuum evaporation.
Decorative PVD systems may use titanium nitride, zirconium nitride, chromium compounds, and other engineered materials to create gold-like yellow, black, gunmetal, gray, brown, or blue finishes. Depending on the coating chemistry and deposition parameters, these films can provide high surface hardness and improved resistance to abrasion.
However, PVD is not one standardized finish with a fixed lifespan. Its performance depends on the substrate alloy, polishing and cleaning quality, soldering materials, coating chemistry, film thickness, process temperature, chamber parameters, fixture design, and any intermediate layers beneath the final film.
This is especially important in jewelry manufacturing because a PVD film closely follows the surface beneath it. Polishing marks, pits, porosity, and other substrate defects may remain visible after coating and can become local weak points. A hard film applied over a soft, flexible, or poorly prepared structure may still crack, peel, or fail around exposed edges.
PVD performance should therefore be validated on the actual jewelry design. A successful result on a rigid pendant does not automatically prove that the same structure will perform equally well on an adjustable ring, thin chain, or hinged component.
Does Gold-Colored PVD Contain Real Gold?
Not necessarily.
Many gold-colored PVD finishes use titanium- or zirconium-based compounds that resemble yellow gold but do not contain a genuine 14K or 18K gold layer. Other systems may deposit genuine gold through PVD or combine electroplated gold with a PVD process.
The supplier should therefore state whether the visible finish is a non-gold compound, a genuine-gold PVD film, an electroplated gold-alloy layer, or a multilayer system combining electroplating and PVD.
A gold-like color alone does not justify descriptions such as “14K gold plated,” “18K gold plated” or “gold vermeil.” These claims must reflect the material actually deposited, its fineness, thickness, and surface coverage.
What Is Traditional Electroplating?
Electroplating is an electrochemical process in which an electrical current deposits a metal or metal alloy onto a conductive jewelry surface from a plating solution.
In jewelry production, electroplating may be used to deposit copper, nickel or nickel-free alternatives, white bronze, palladium, silver, gold alloys, and rhodium. Its purpose is not limited to adding a visible color. Different electroplated layers can improve surface smoothness, brightness, adhesion, corrosion resistance, and resistance to metal diffusion.
A brass jewelry product, for example, may use copper to improve surface leveling, a palladium or white-bronze layer as a diffusion barrier, and gold or another decorative coating as the visible finish. A PVD film may then be added when the product requires an engineered color or a harder final surface.
A representative structure could therefore be
PVD or protective top layer → decorative metal or color layer → diffusion barrier → copper leveling layer → brass base
This is only an example. There is no universal layer structure suitable for every brass or sterling silver product. The correct sequence depends on the alloy, product design, required color, restricted-substance requirements, and expected wearing conditions.
PVD vs Electroplating: Technical and Commercial Comparison
|
Decision Factor |
PVD Coating |
Traditional Electroplating |
|
Deposition environment |
Vacuum chamber |
Liquid plating bath |
|
Typical coating materials |
Metals, nitrides, carbides, oxides and engineered compounds |
Gold, silver, rhodium, palladium, copper and other metals or alloys |
|
Genuine gold content |
May or may not contain genuine gold |
Can deposit a specified genuine gold or gold-alloy layer |
|
Surface hardness |
Hard nitride and ceramic-type films are available |
Depends on the deposited metal, alloy and complete layer structure |
|
Surface leveling |
Closely follows the prepared substrate |
Copper and other layers can improve smoothness and brightness |
|
Recessed geometry |
Coverage depends heavily on source position, rotation and fixture design |
Immersion provides broader access, although current distribution still affects thickness |
|
Flexible products |
Hard films may require additional bend and flex validation |
Metallic layers may be more accommodating, depending on alloy and thickness |
|
Color range |
Strong for black, gunmetal and engineered decorative colors |
Strong for genuine precious-metal and alloy-specific colors |
|
Main cost drivers |
Chamber setup, fixture design, coating chemistry, batch utilization and pretreatment |
Precious-metal price, karat, thickness, underlayers, bath control and finishing |
|
Typical purpose |
Hard decorative and engineered surfaces |
Precious-metal deposition, leveling, barriers and complex conductive shapes |
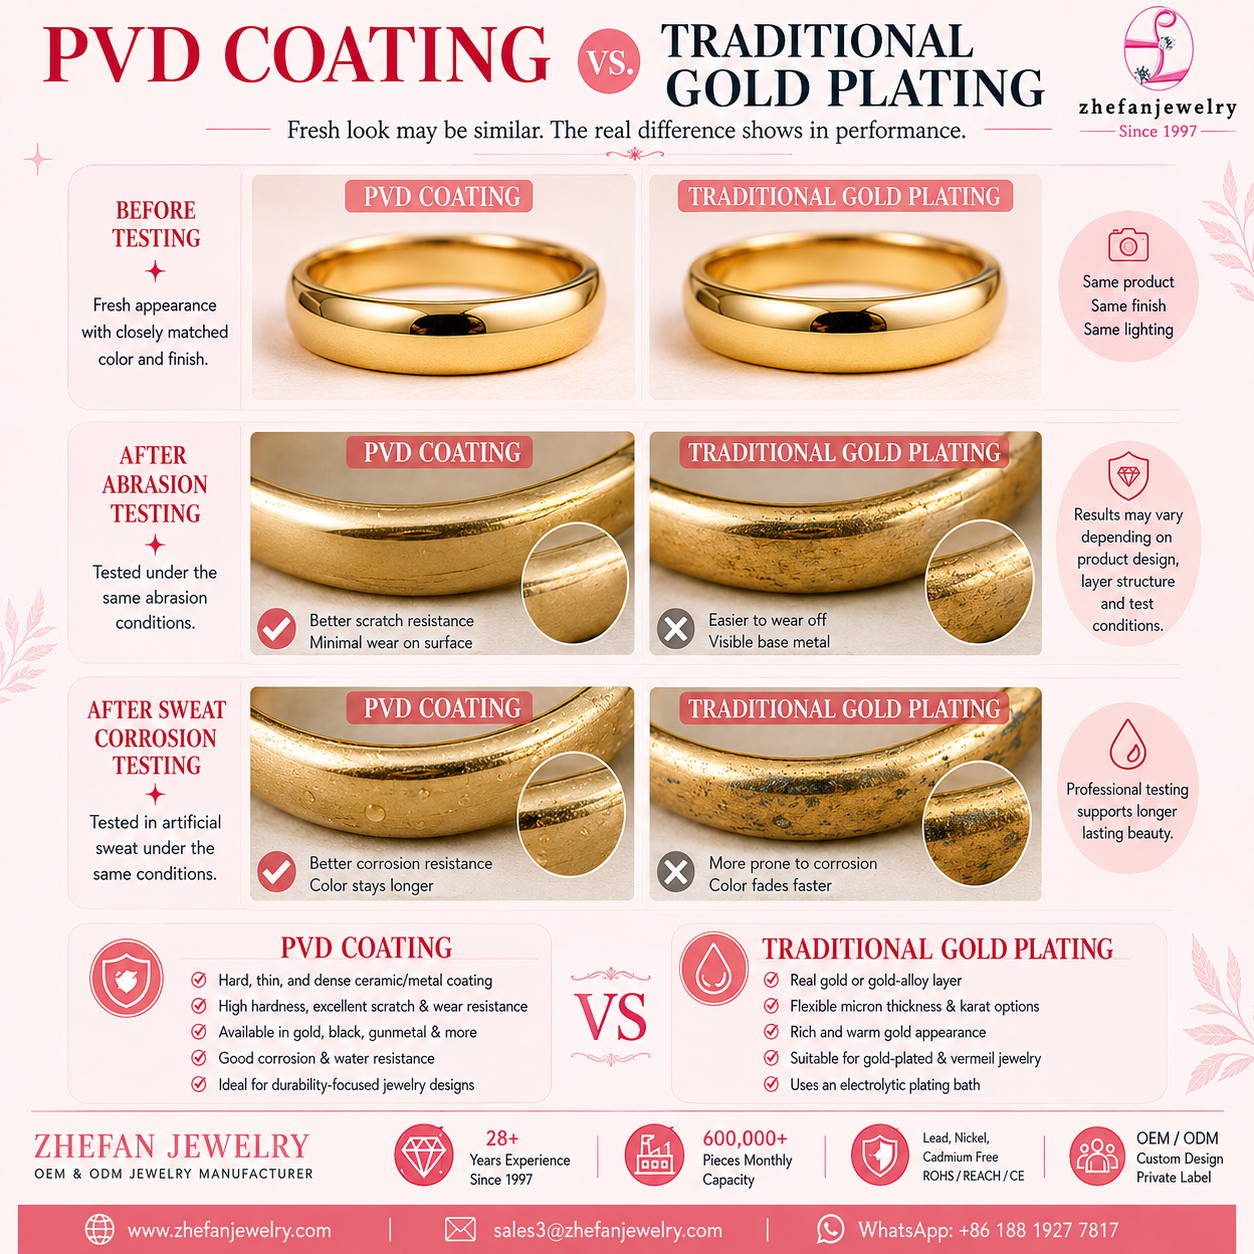
The two processes should not be compared only by micron thickness. A thin, hard PVD film and a thicker electroplated gold layer may serve different engineering and commercial purposes.
From a sourcing perspective, the buyer should examine the complete coating material, layer sequence, adhesion, porosity, surface preparation, product flexibility, and intended marketing claims. A single thickness figure without information about the measured layer and underlying construction is not enough to evaluate quality
Which Process Is More Durable?
A correctly engineered hard PVD film may provide better abrasion resistance than a very thin decorative gold layer. This makes PVD attractive for rigid jewelry surfaces exposed to regular friction.
However, hardness alone does not determine the service life of a finished product. Adhesion between layers, substrate flexibility, coating porosity, exposed edges, soldering points, product deformation, and chemical exposure all influence performance. Contact with sweat, perfume, chlorine, saltwater, and cleaning products can also accelerate surface changes.
A hard coating on a soft adjustable ring may experience concentrated stress every time the ring is opened or closed. A chain or clasp may fail differently from a pendant because the coating is repeatedly flexed or rubbed at connecting points. Product structure must therefore be considered together with the coating properties.
Electroplated jewelry can also achieve strong performance when it uses proper polishing, suitable barrier layers, controlled precious-metal thickness, and an appropriate protective topcoat. It is therefore inaccurate to state that every PVD-coated product will last longer than every electroplated product.
Are PVD and Electroplated Jewelry Waterproof?
Both processes can improve resistance to moisture and corrosion, but neither should automatically be described as permanently waterproof, corrosion-proof, tarnish-proof, or guaranteed never to fade.
Thin coatings may contain microscopic pores or become damaged at high-friction areas and exposed edges. Once sweat, water, or chemicals reach the substrate, discoloration or corrosion may begin.
Claims such as “water resistant” should be supported by a defined test method, specified exposure conditions, and clear acceptance criteria. Even then, laboratory results should be presented as evidence under controlled conditions rather than as a universal guarantee of permanent color retention.
PVD and Electroplating on Brass and 925 Sterling Silver
Brass Jewelry
Brass is widely used in demi-fine and fashion jewelry because it supports casting, machining, polishing, stone setting, and complex design development. Its copper and zinc content, however, makes surface preparation and barrier-layer design particularly important.
Without an effective barrier structure, moisture and chemicals may contribute to oxidation, discoloration, or diffusion from the base metal. For this reason, many brass jewelry systems use electroplated leveling and barrier layers before the visible decorative finish is applied.
PVD may be considered as the final surface when the design requires a harder finish or an engineered color. However, the correct structure still depends on the brass alloy, polishing quality, soldering locations, stone setting, nickel requirements, product rigidity, and target performance.
Direct PVD deposition on bare brass may be technically possible in selected applications, but it should not automatically be treated as the most reliable mass-production solution. Design-specific sample development and testing are recommended before a bulk order is approved.
925 Sterling Silver Jewelry
Selected 925 sterling silver jewelry can also receive PVD coating. Feasibility depends on the silver alloy, surface oxidation, soldering materials, polishing quality, product thickness, stones, adhesives, and the temperature or vacuum sensitivity of the design.
PVD can be appropriate for sterling silver products requiring black, gunmetal, or other engineered finishes. Flexible and movable designs require additional attention because mechanical deformation may place stress on a hard coating.
When a sterling silver product is intended to be marketed as gold vermeil, the coating system must still meet the applicable requirements for genuine gold content, fineness, thickness, and significant-surface coverage. A titanium nitride or zirconium nitride layer does not become gold vermeil simply because it is deposited over sterling silver.
Based on Zhefan Jewelry’s production experience, rigid earrings, pendants, and solid bangles are generally easier to evaluate for PVD than highly flexible chains, thin adjustable rings, or products containing multiple soldering points. For new designs, our engineering team reviews the alloy, polishing, stone-setting sequence, and movement areas before recommending a coating structure.
Gold-Plated and Gold-Vermeil Requirements in the United States
The U.S. Federal Trade Commission’s Guides for the Jewelry, Precious Metals, and Pewter Industries, published under 16 CFR Part 23, address potentially misleading descriptions of precious-metal products.
Under the FTC Jewelry Guides, the term "vermeil" applies to a product with a sterling silver base that is coated on all significant surfaces with gold or a gold alloy of at least 10-karat fineness. The coating must have reasonable durability and a minimum thickness equivalent to 2.5 microns of fine gold.
If a base-metal layer is applied over the sterling silver before the gold layer, the presence of that intermediate layer may require disclosure. The FTC guidance also makes clear that marketers should not misrepresent the karat fineness, thickness, surface coverage, or application method of a gold coating.
The current FTC guidance provides an example in which a product electroplated with gold or a gold alloy of at least 10-karat fineness and a minimum thickness equivalent to 0.175 microns of fine gold may be described using qualifying gold-plating terminology, provided the coating has reasonable durability and appropriate surface coverage.
Official sources:
FTC: Jewelry, Precious Metals, and Pewter Industries—16 CFR Part 23
FTC: Statement of Basis and Purpose for the Revised Jewelry Guides
From a B2B purchasing perspective, the term “gold plated” should not be approved solely because a product is gold-colored. Buyers should obtain written confirmation of the deposited material, gold fineness, thickness, measurement location, surface coverage, and any intermediate layers.
EU REACH Requirements for Jewelry
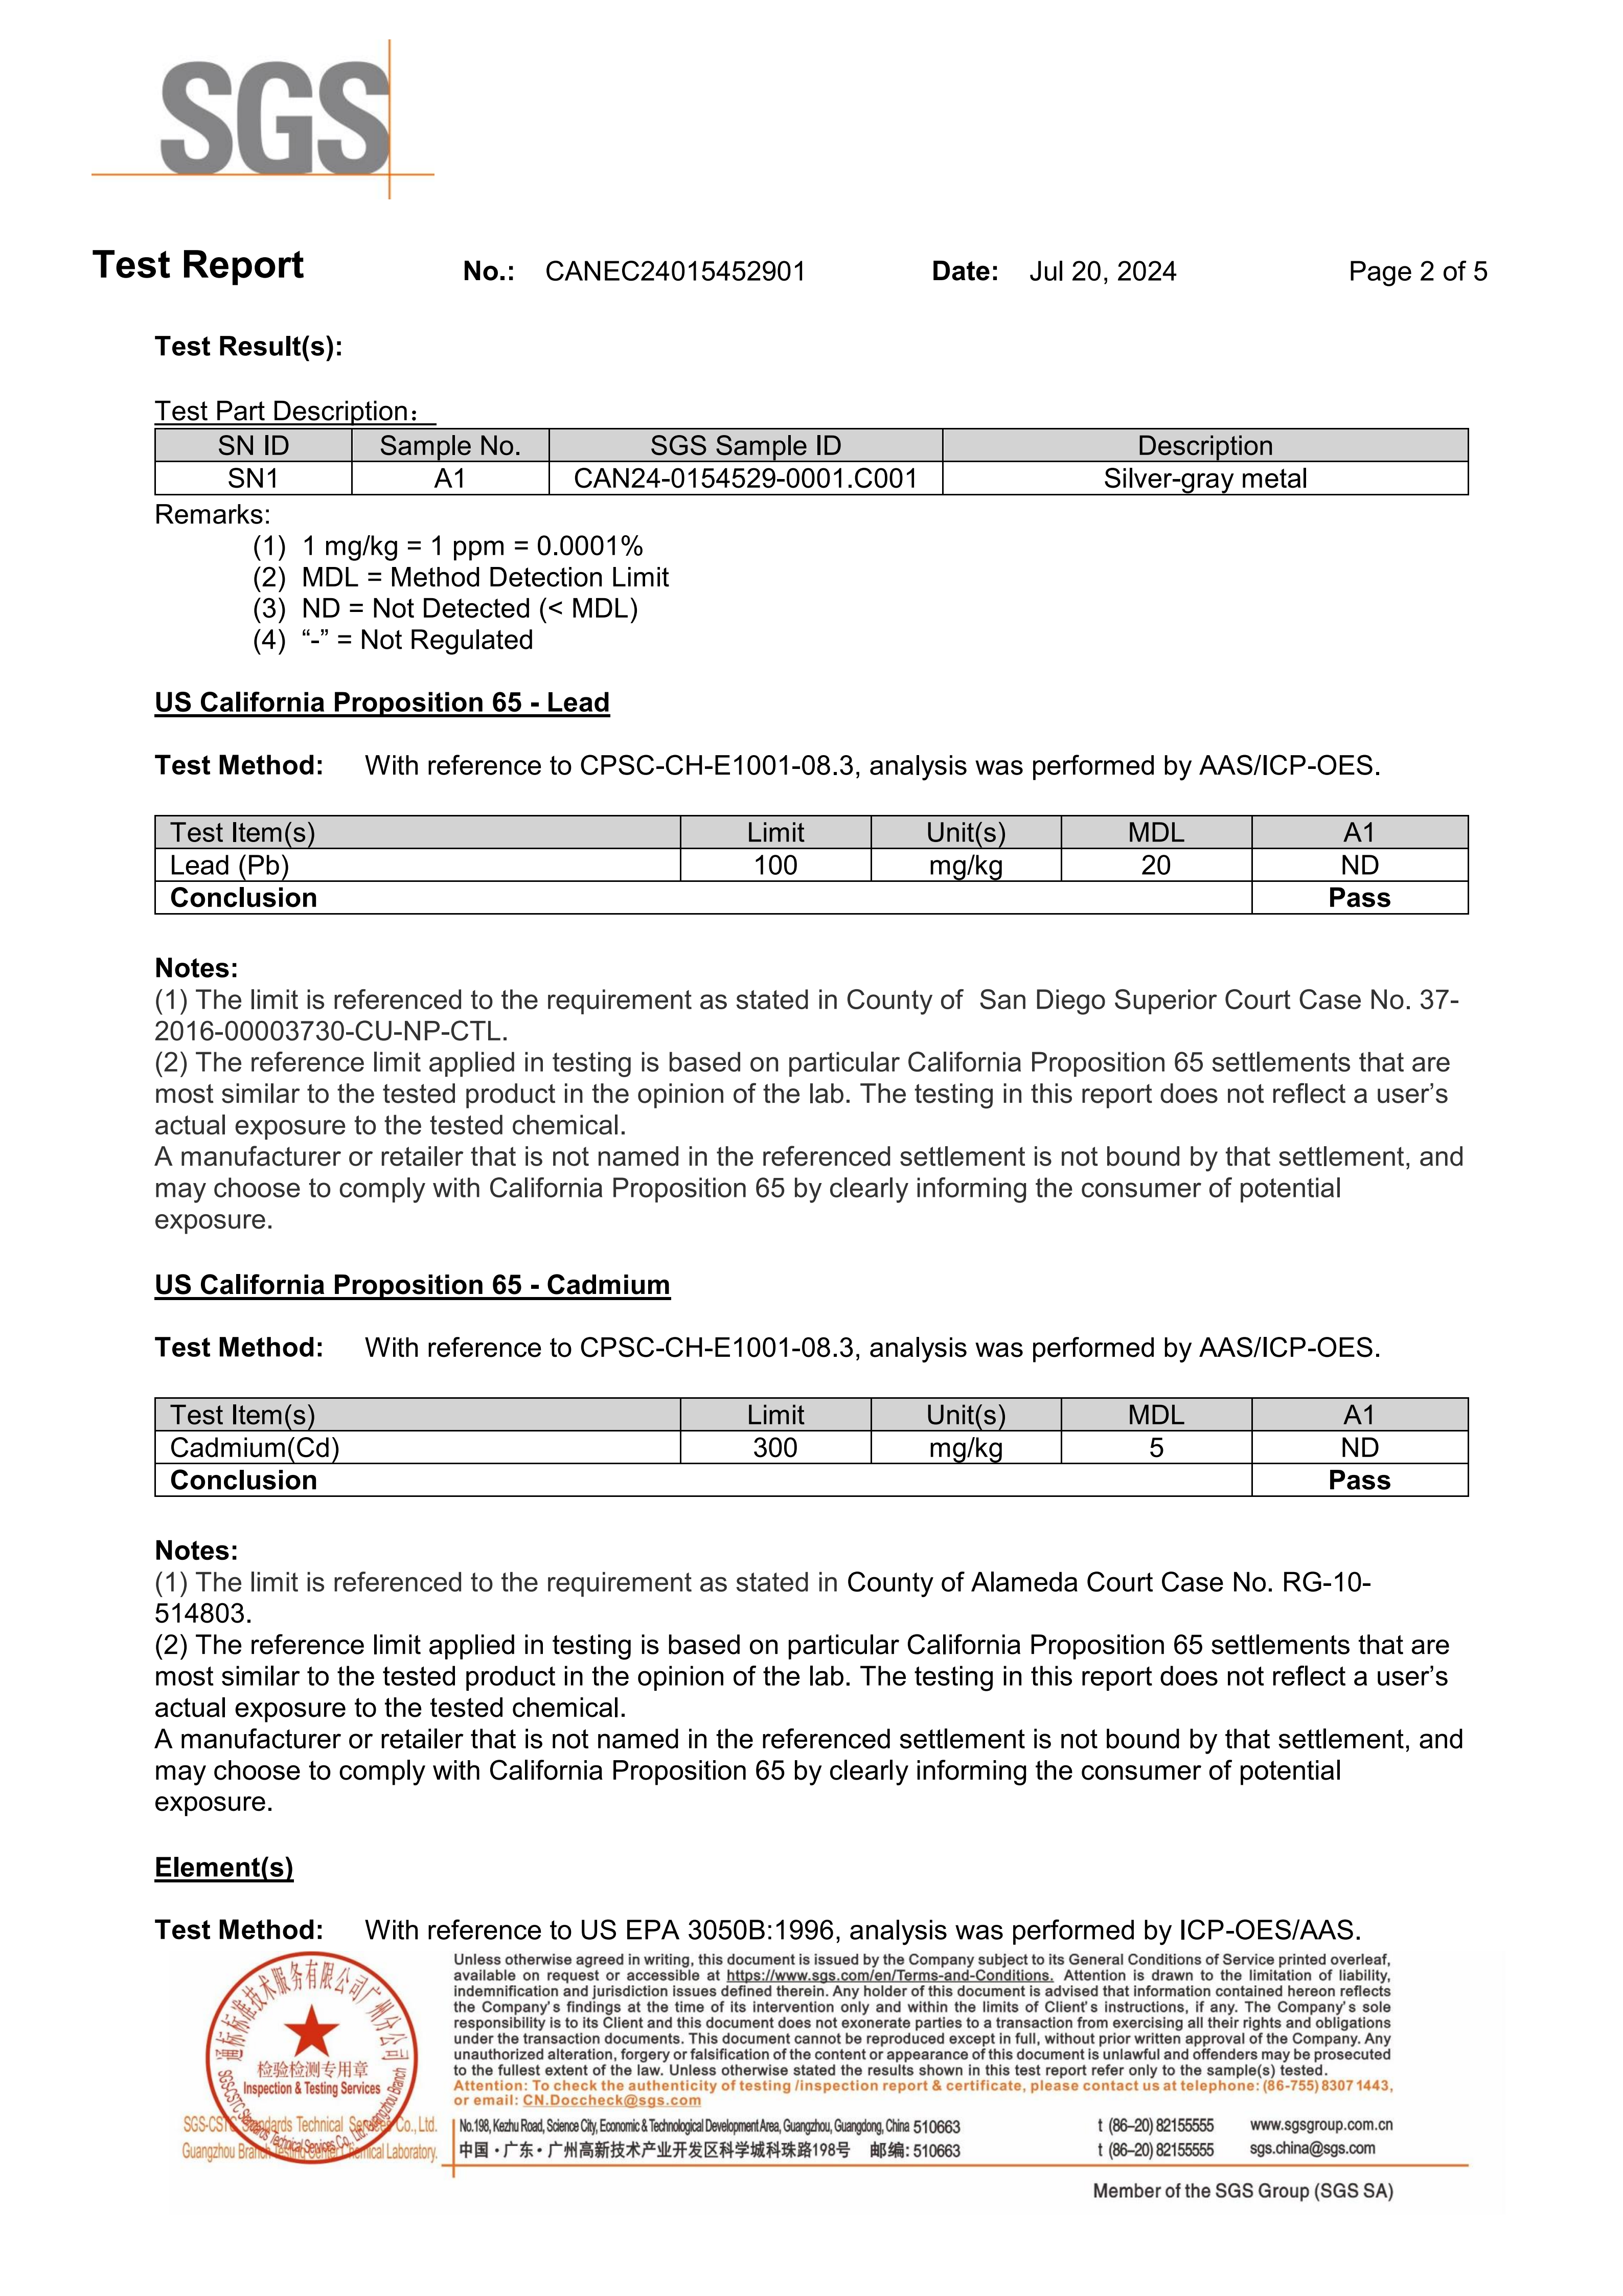
Jewelry sold in the European Union may be subject to restrictions under Regulation (EC) No. 1907/2006, commonly known as REACH. The consolidated text available through EUR-Lex includes jewelry-related restrictions in Annex XVII, particularly Entry 23 for cadmium, Entry 27 for nickel, and Entry 63 for lead.
Under the nickel restriction, articles inserted into pierced parts of the human body are subject to a release limit of 0.2 μg/cm²/week, while articles intended to come into direct and prolonged contact with the skin are subject to a limit of 0.5 μg/cm²/week. For coated articles, the surface treatment must remain sufficiently effective during the defined period of normal use.
The European Commission has referenced EN 1811:2023 as the test method for determining nickel release from piercing posts and articles intended for direct and prolonged skin contact. For coated items, EN 12472:2020 provides an accelerated wear and corrosion procedure that may be used before nickel-release testing.
Official sources:
EUR-Lex: Consolidated REACH Regulation
EUR-Lex: Commission Communication C/2023/1604—EN 1811 and EN 12472 References
REACH Annex XVI I also restrict lead in individual jewelry parts at concentrations equal to or greater than 0.05% by weight, subject to specified definitions and exemptions. Cadmium is generally restricted at concentrations equal to or greater than 0.01% by weight in relevant metal parts of jewelry and imitation jewelry.
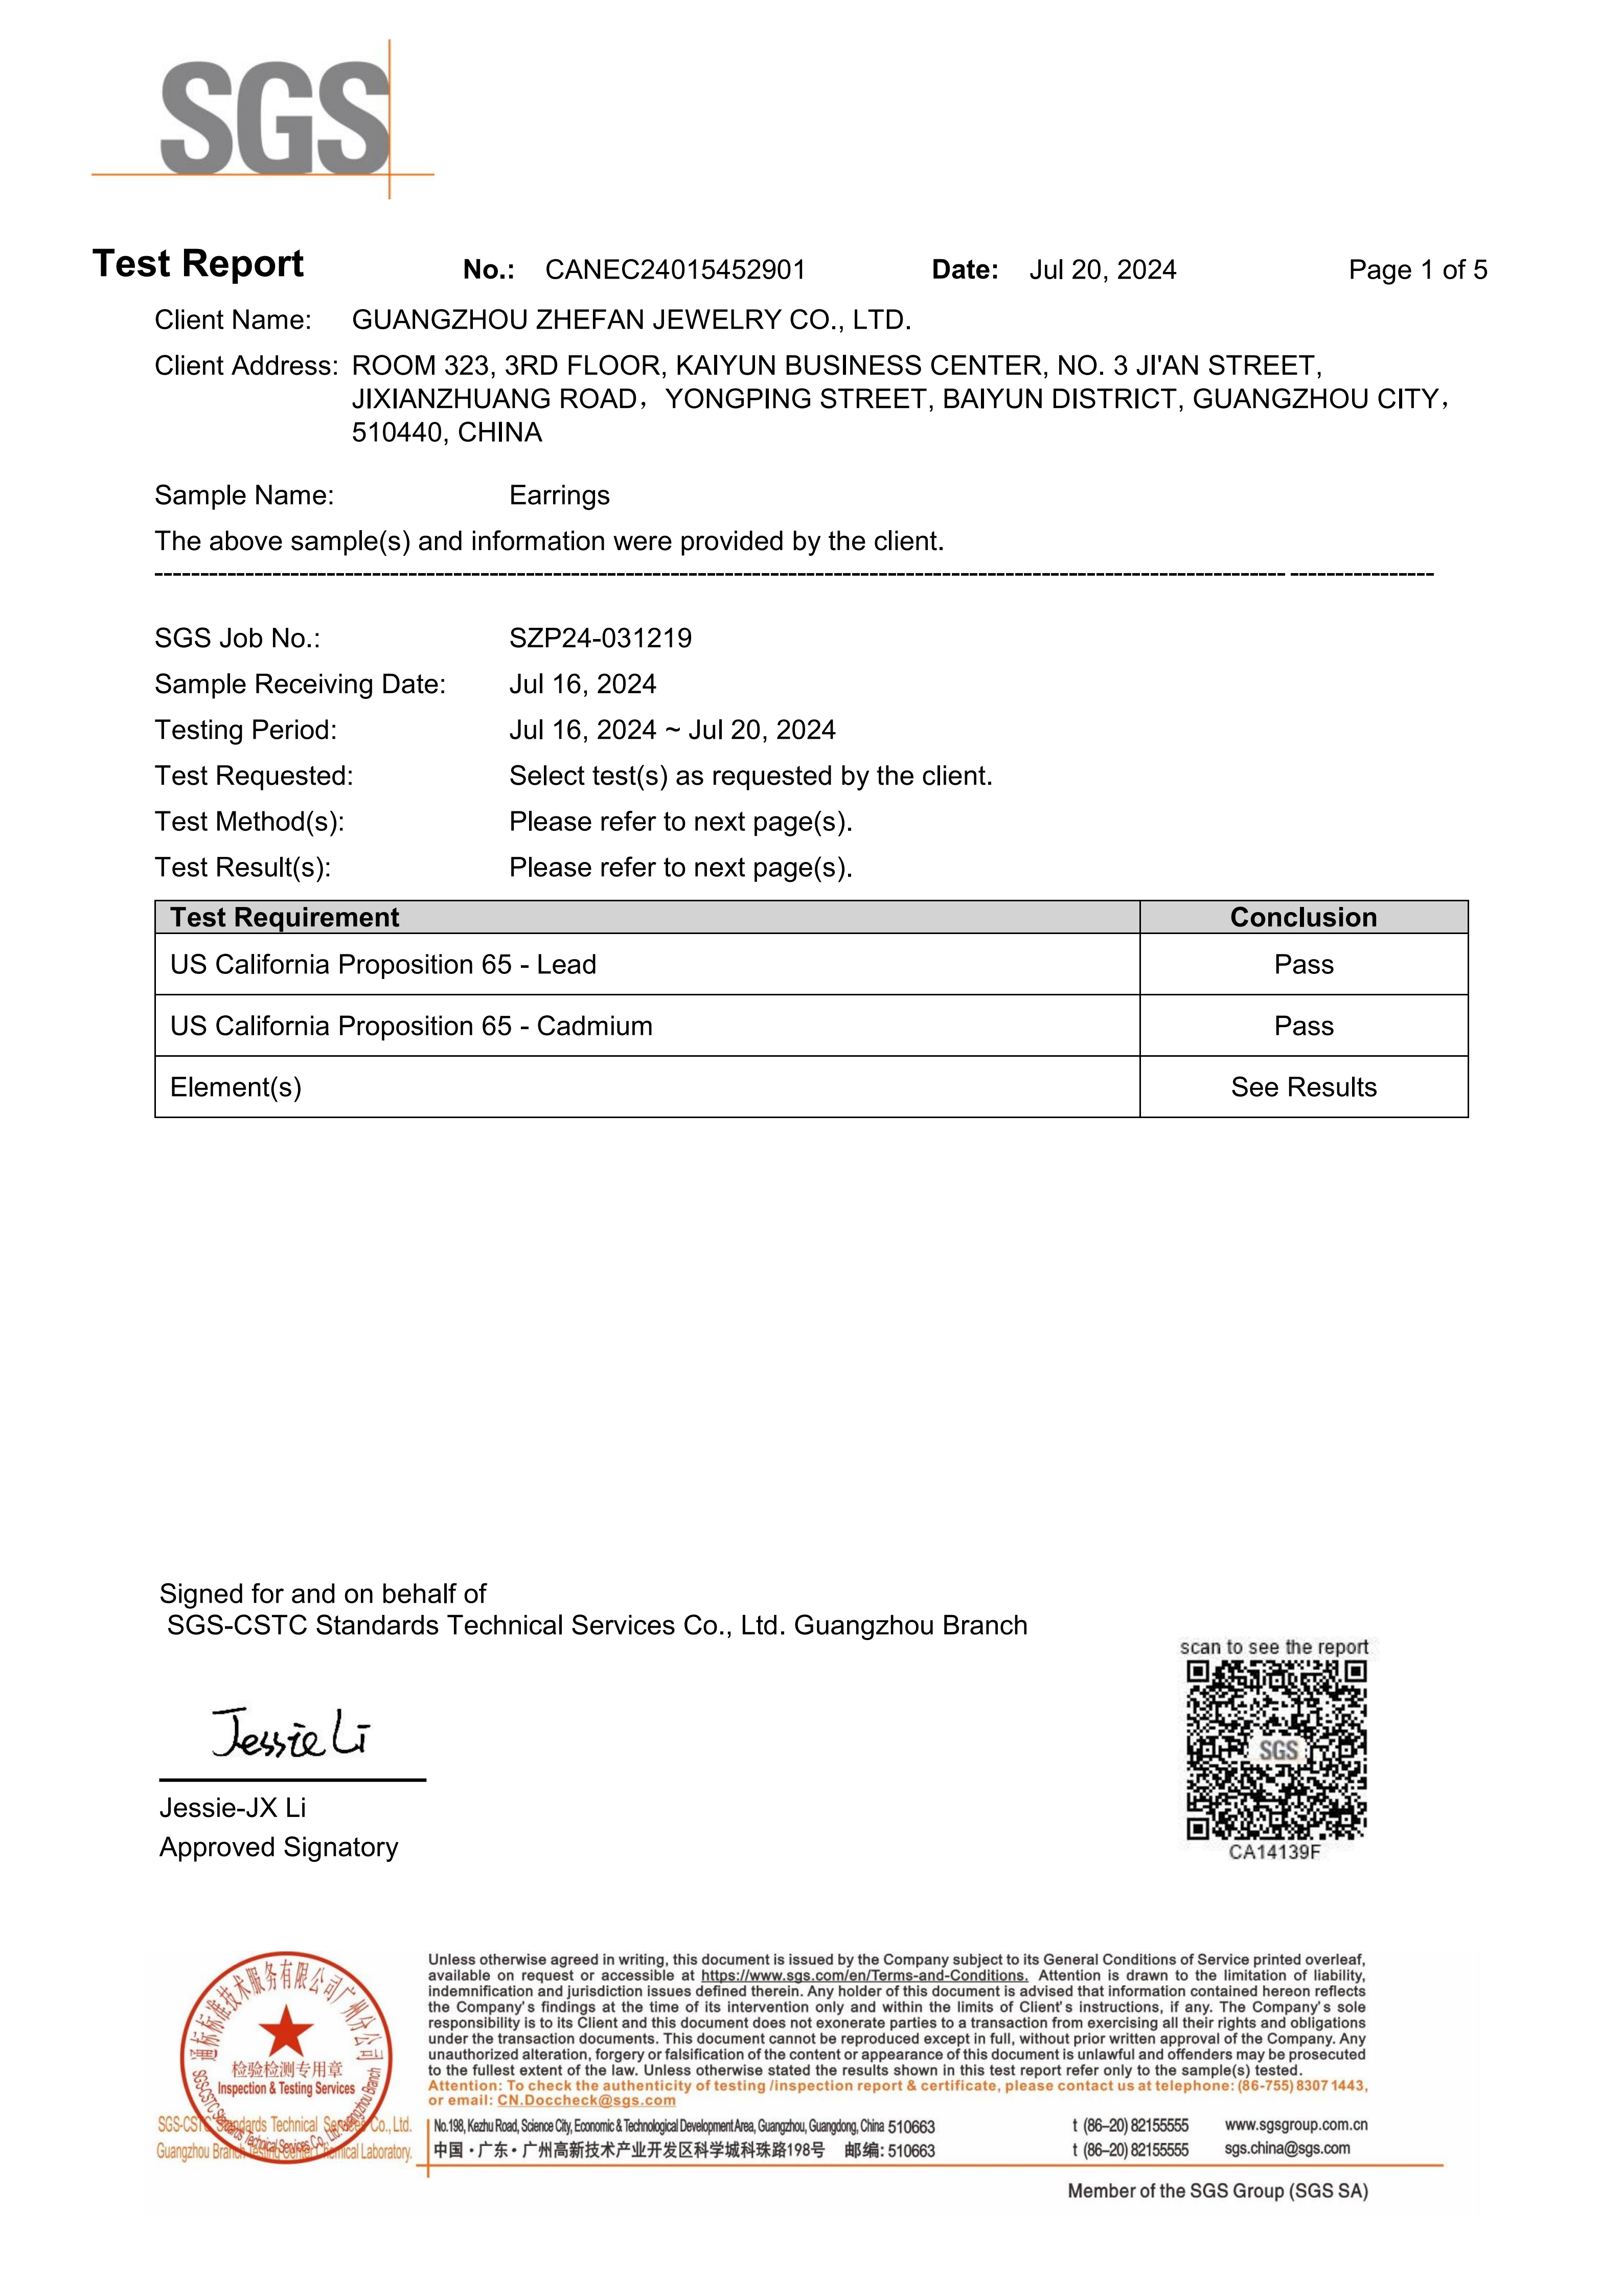
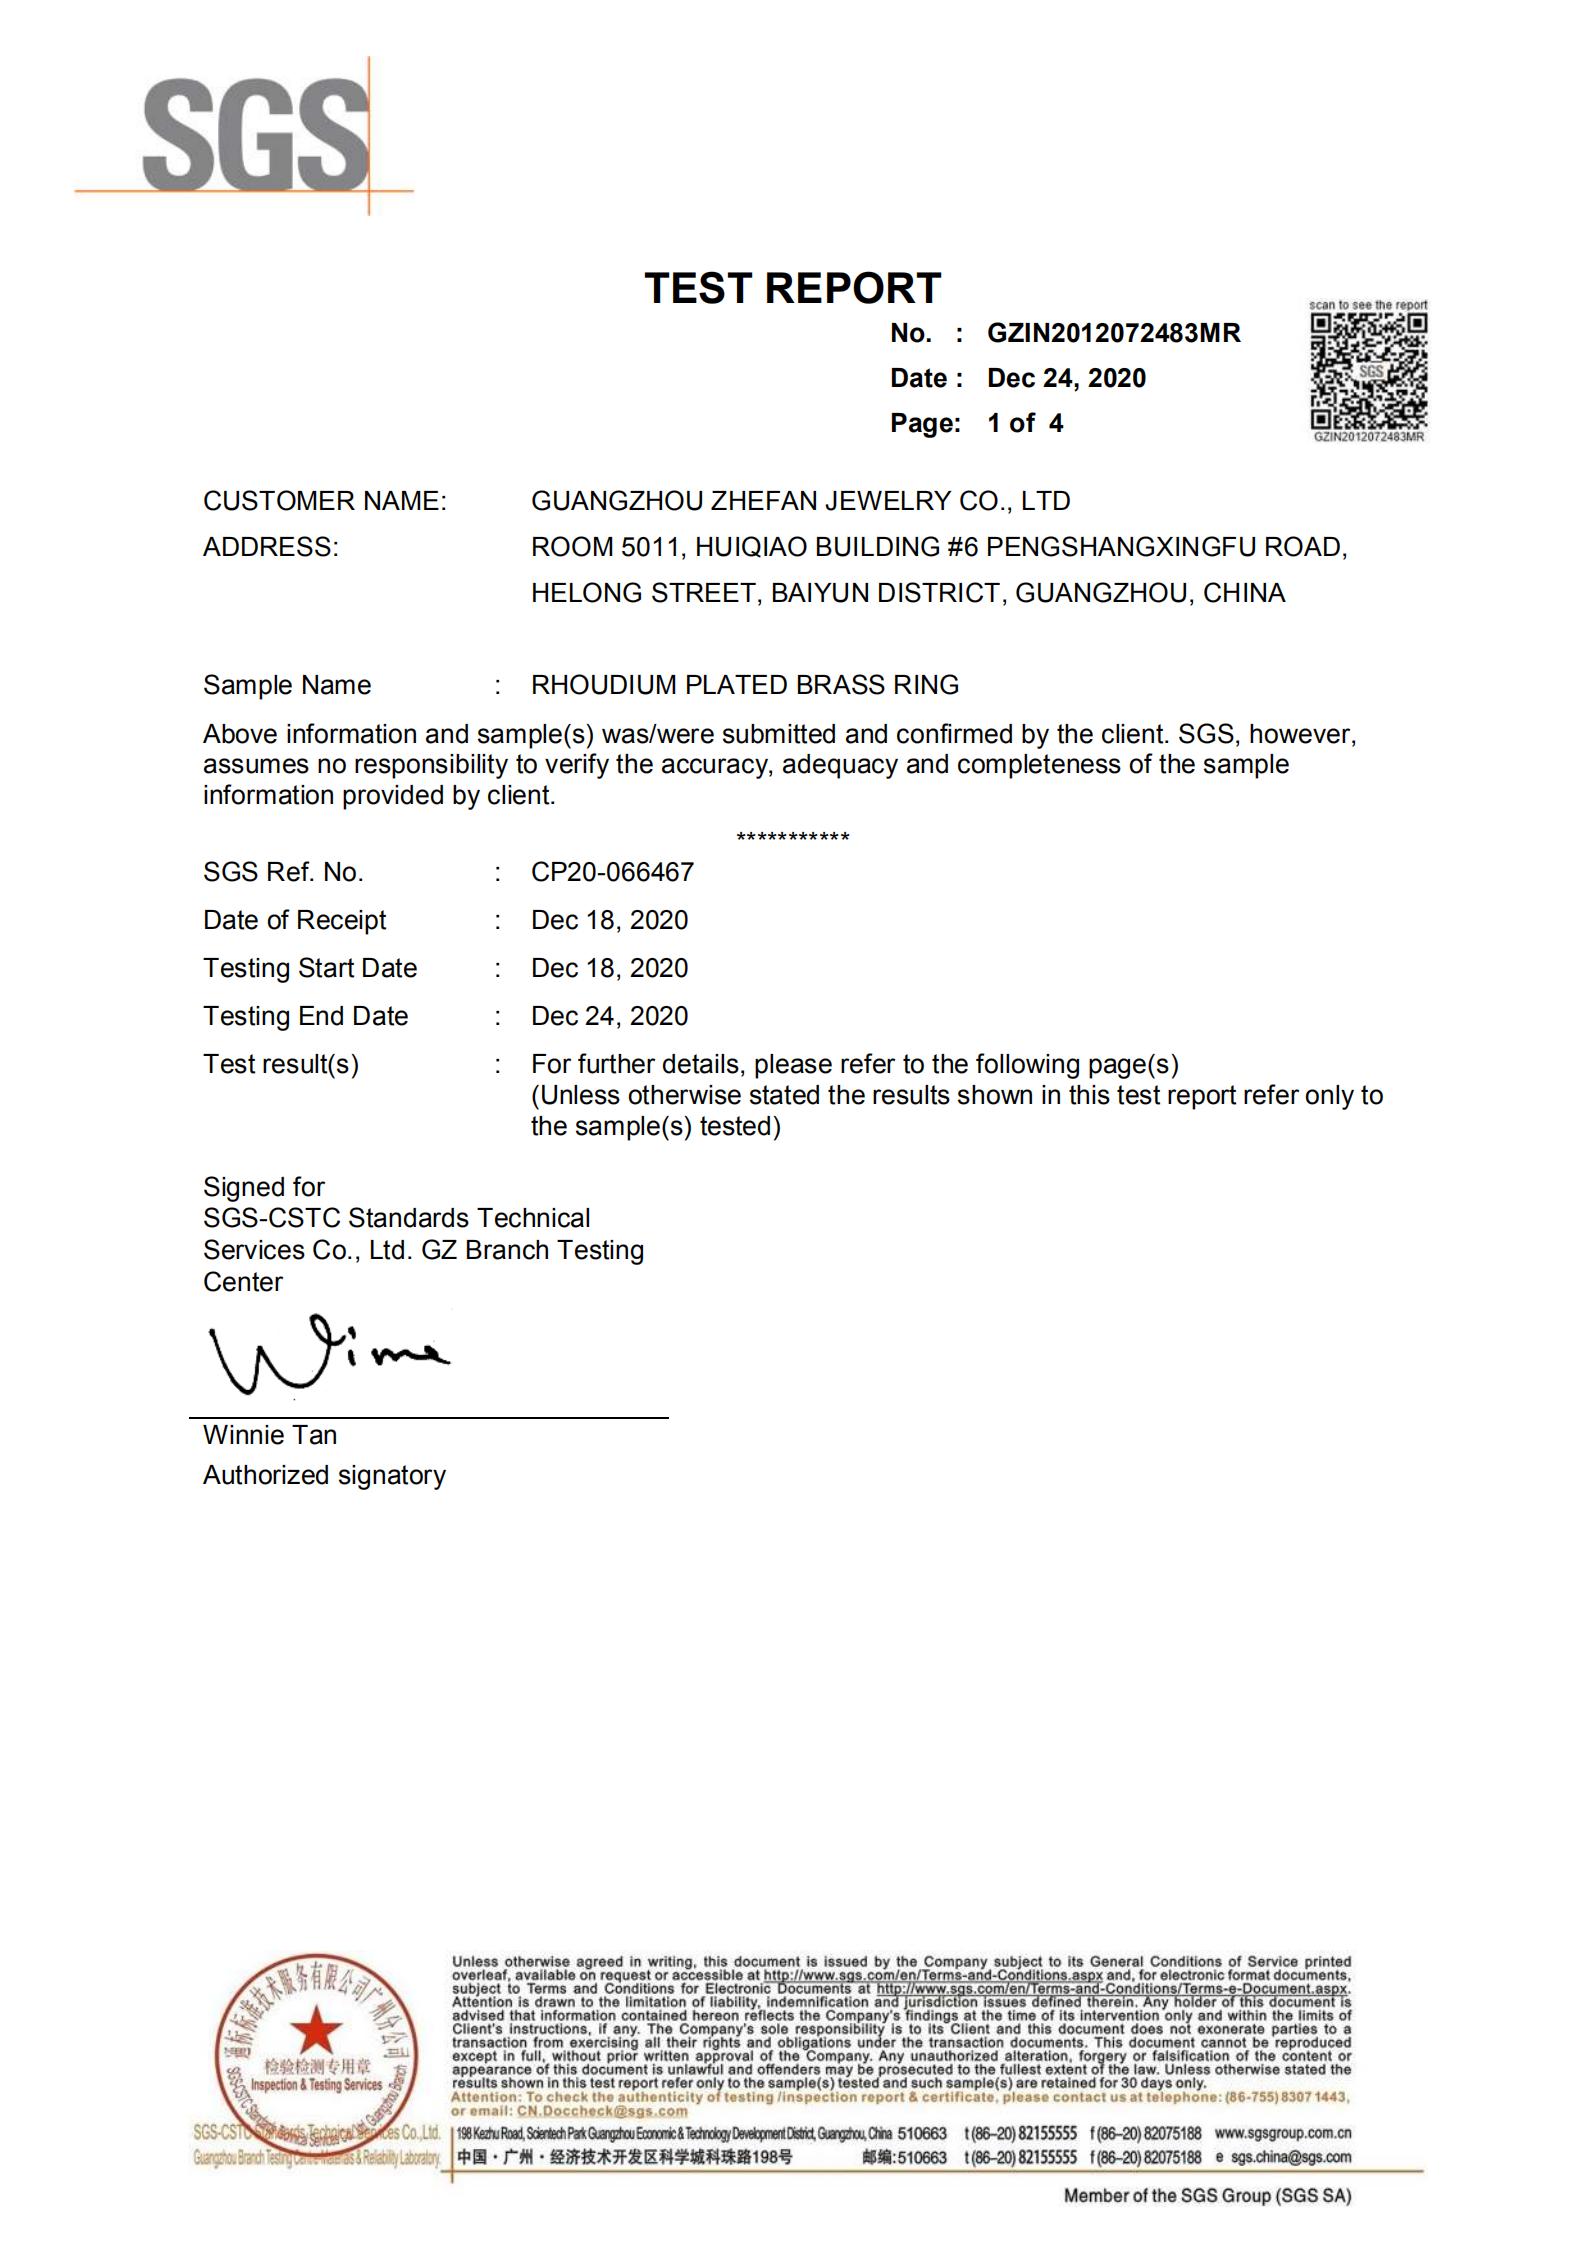
A supplier statement such as “nickel-free,” "lead-free," or “cadmium-free” should therefore be supported by a report that covers the correct product, material, or representative construction. Testing only the base alloy does not necessarily demonstrate compliance of the complete finished article, particularly when solder, intermediate layers, stones, or other components are present.
Regulations and referenced standards may be amended. Buyers should confirm the applicable version and destination-market requirements with an accredited laboratory or qualified compliance specialist before placing a product on the market.
Testing and Acceptance Criteria for B2B Orders
A professional purchase specification should define the test method, sample quantity, measurement location, exposure duration, and pass-or-fail criteria. Stating only “XRF required” or “salt spray required” leaves too much room for inconsistent interpretation.
|
Test or Inspection |
Main Purpose |
Important Limitation |
|
XRF coating-thickness measurement |
Measure suitable metallic coating layers non-destructively |
Accuracy depends on calibration, geometry, substrate, layer combination and measurement position |
|
Adhesion testing |
Identify peeling, lifting or separation between coating and substrate |
The selected test must match the coating, substrate and expected product use |
|
Salt-spray testing |
Reveal corrosion weaknesses, porosity, discontinuities and coating damage |
Test hours cannot be directly converted into months or years of consumer wear |
|
Nickel-release testing |
Evaluate compliance for EU piercing and skin-contact articles |
Testing should use the finished or appropriately representative article |
|
Restricted-substance testing |
Evaluate lead, cadmium and other regulated substances |
The test scope must match the destination market and product components |
|
Artificial-sweat testing |
Evaluate appearance and corrosion under a controlled sweat environment |
Test conditions do not reproduce every consumer’s sweat chemistry |
|
Abrasion and flex testing |
Evaluate friction, bending and repeated movement |
The method must reflect the actual jewelry category |
XRF Coating-Thickness Measurement
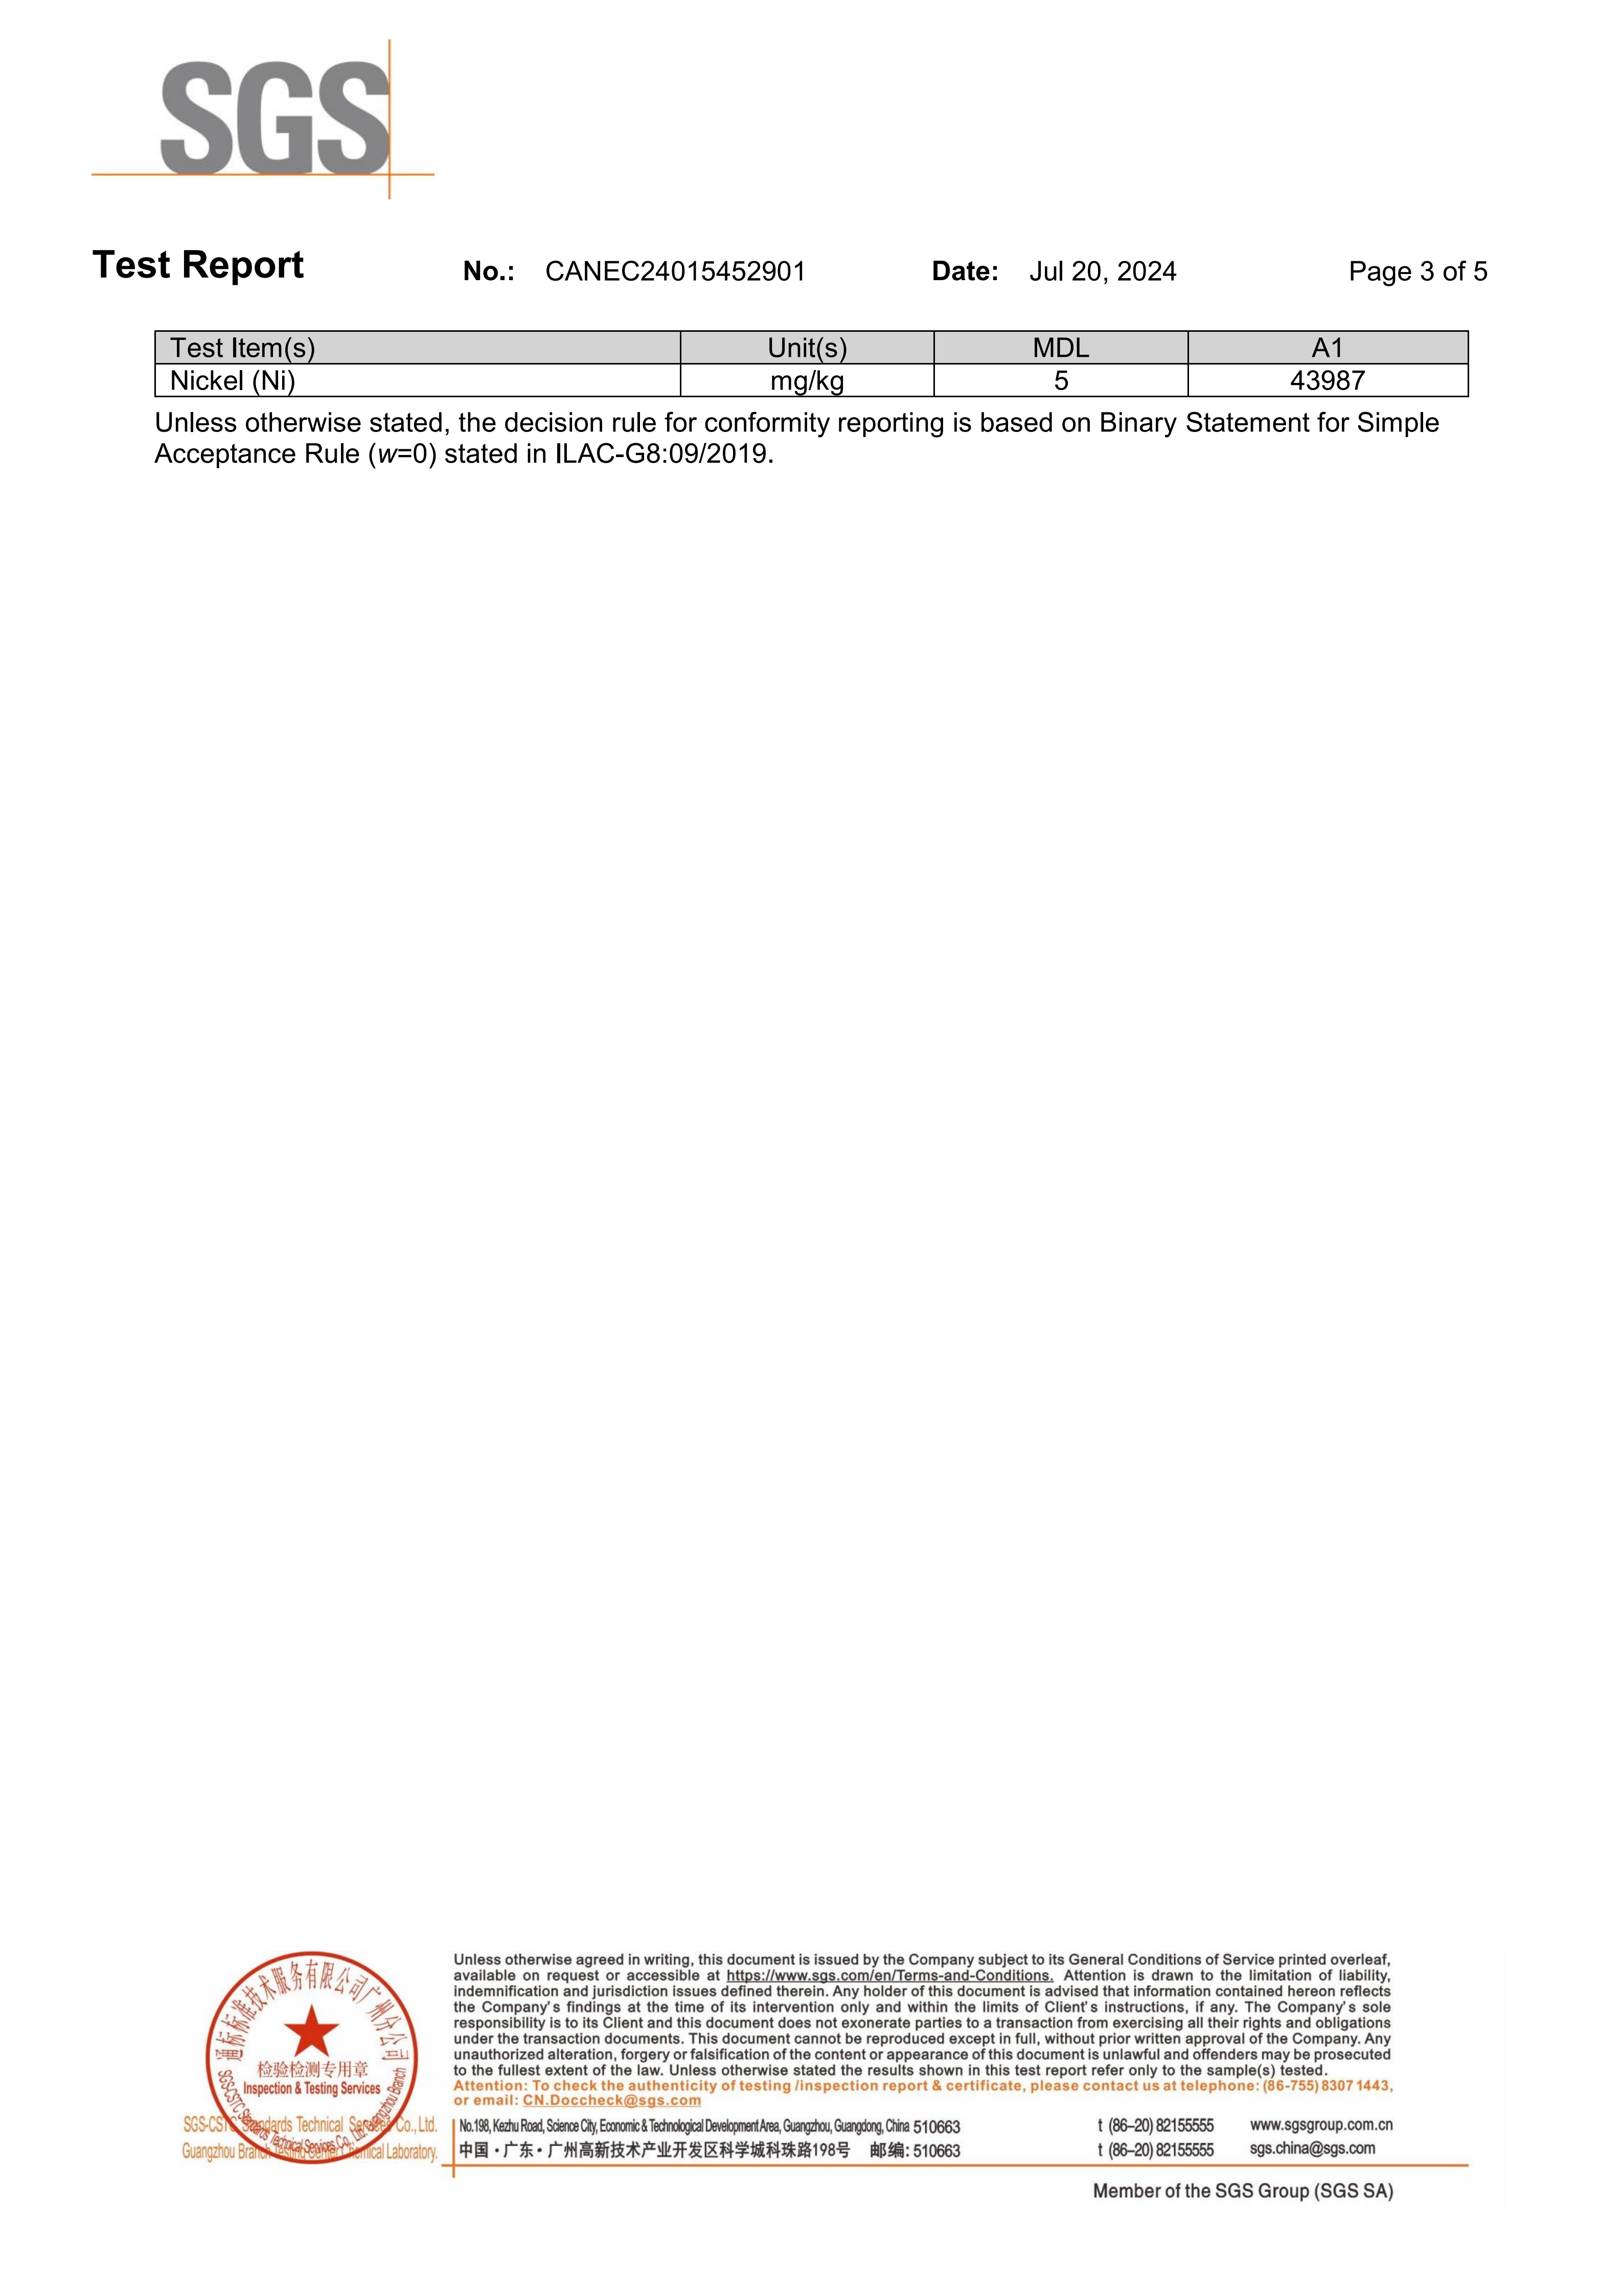
ISO 3497:2000, Metallic Coatings—Measurement of Coating Thickness—X-ray Spectrometric Methods, describes X-ray spectrometric measurement of metallic coating thickness. ISO states that this edition was reviewed and confirmed in 2022 and therefore remains current at the time of writing.
XRF can provide rapid, non-destructive measurements on suitable coating systems, but the result depends on instrument calibration, substrate composition, layer combination, and product geometry. Curved, textured, or very small jewelry surfaces may require special calibration or additional analytical methods.
For meaningful B2B quality control, the specification should identify which layer is being measured, where the measurement is taken, how many readings are required, and what tolerance is acceptable.
Adhesion Testing
ASTM B571-23, Standard Practice for Qualitative Adhesion Testing of Metallic Coatings, covers qualitative methods for evaluating coating adhesion. The standard recognizes that the appropriate test depends on the functional use of the product and that representative test panels may be appropriate when the actual item cannot be tested directly.
This means an adjustable ring, formed component, and rigid pendant may require different approaches. ASTM B571 should not be presented as one universal numerical adhesion value applicable to every jewelry product.
Salt-Spray Testing
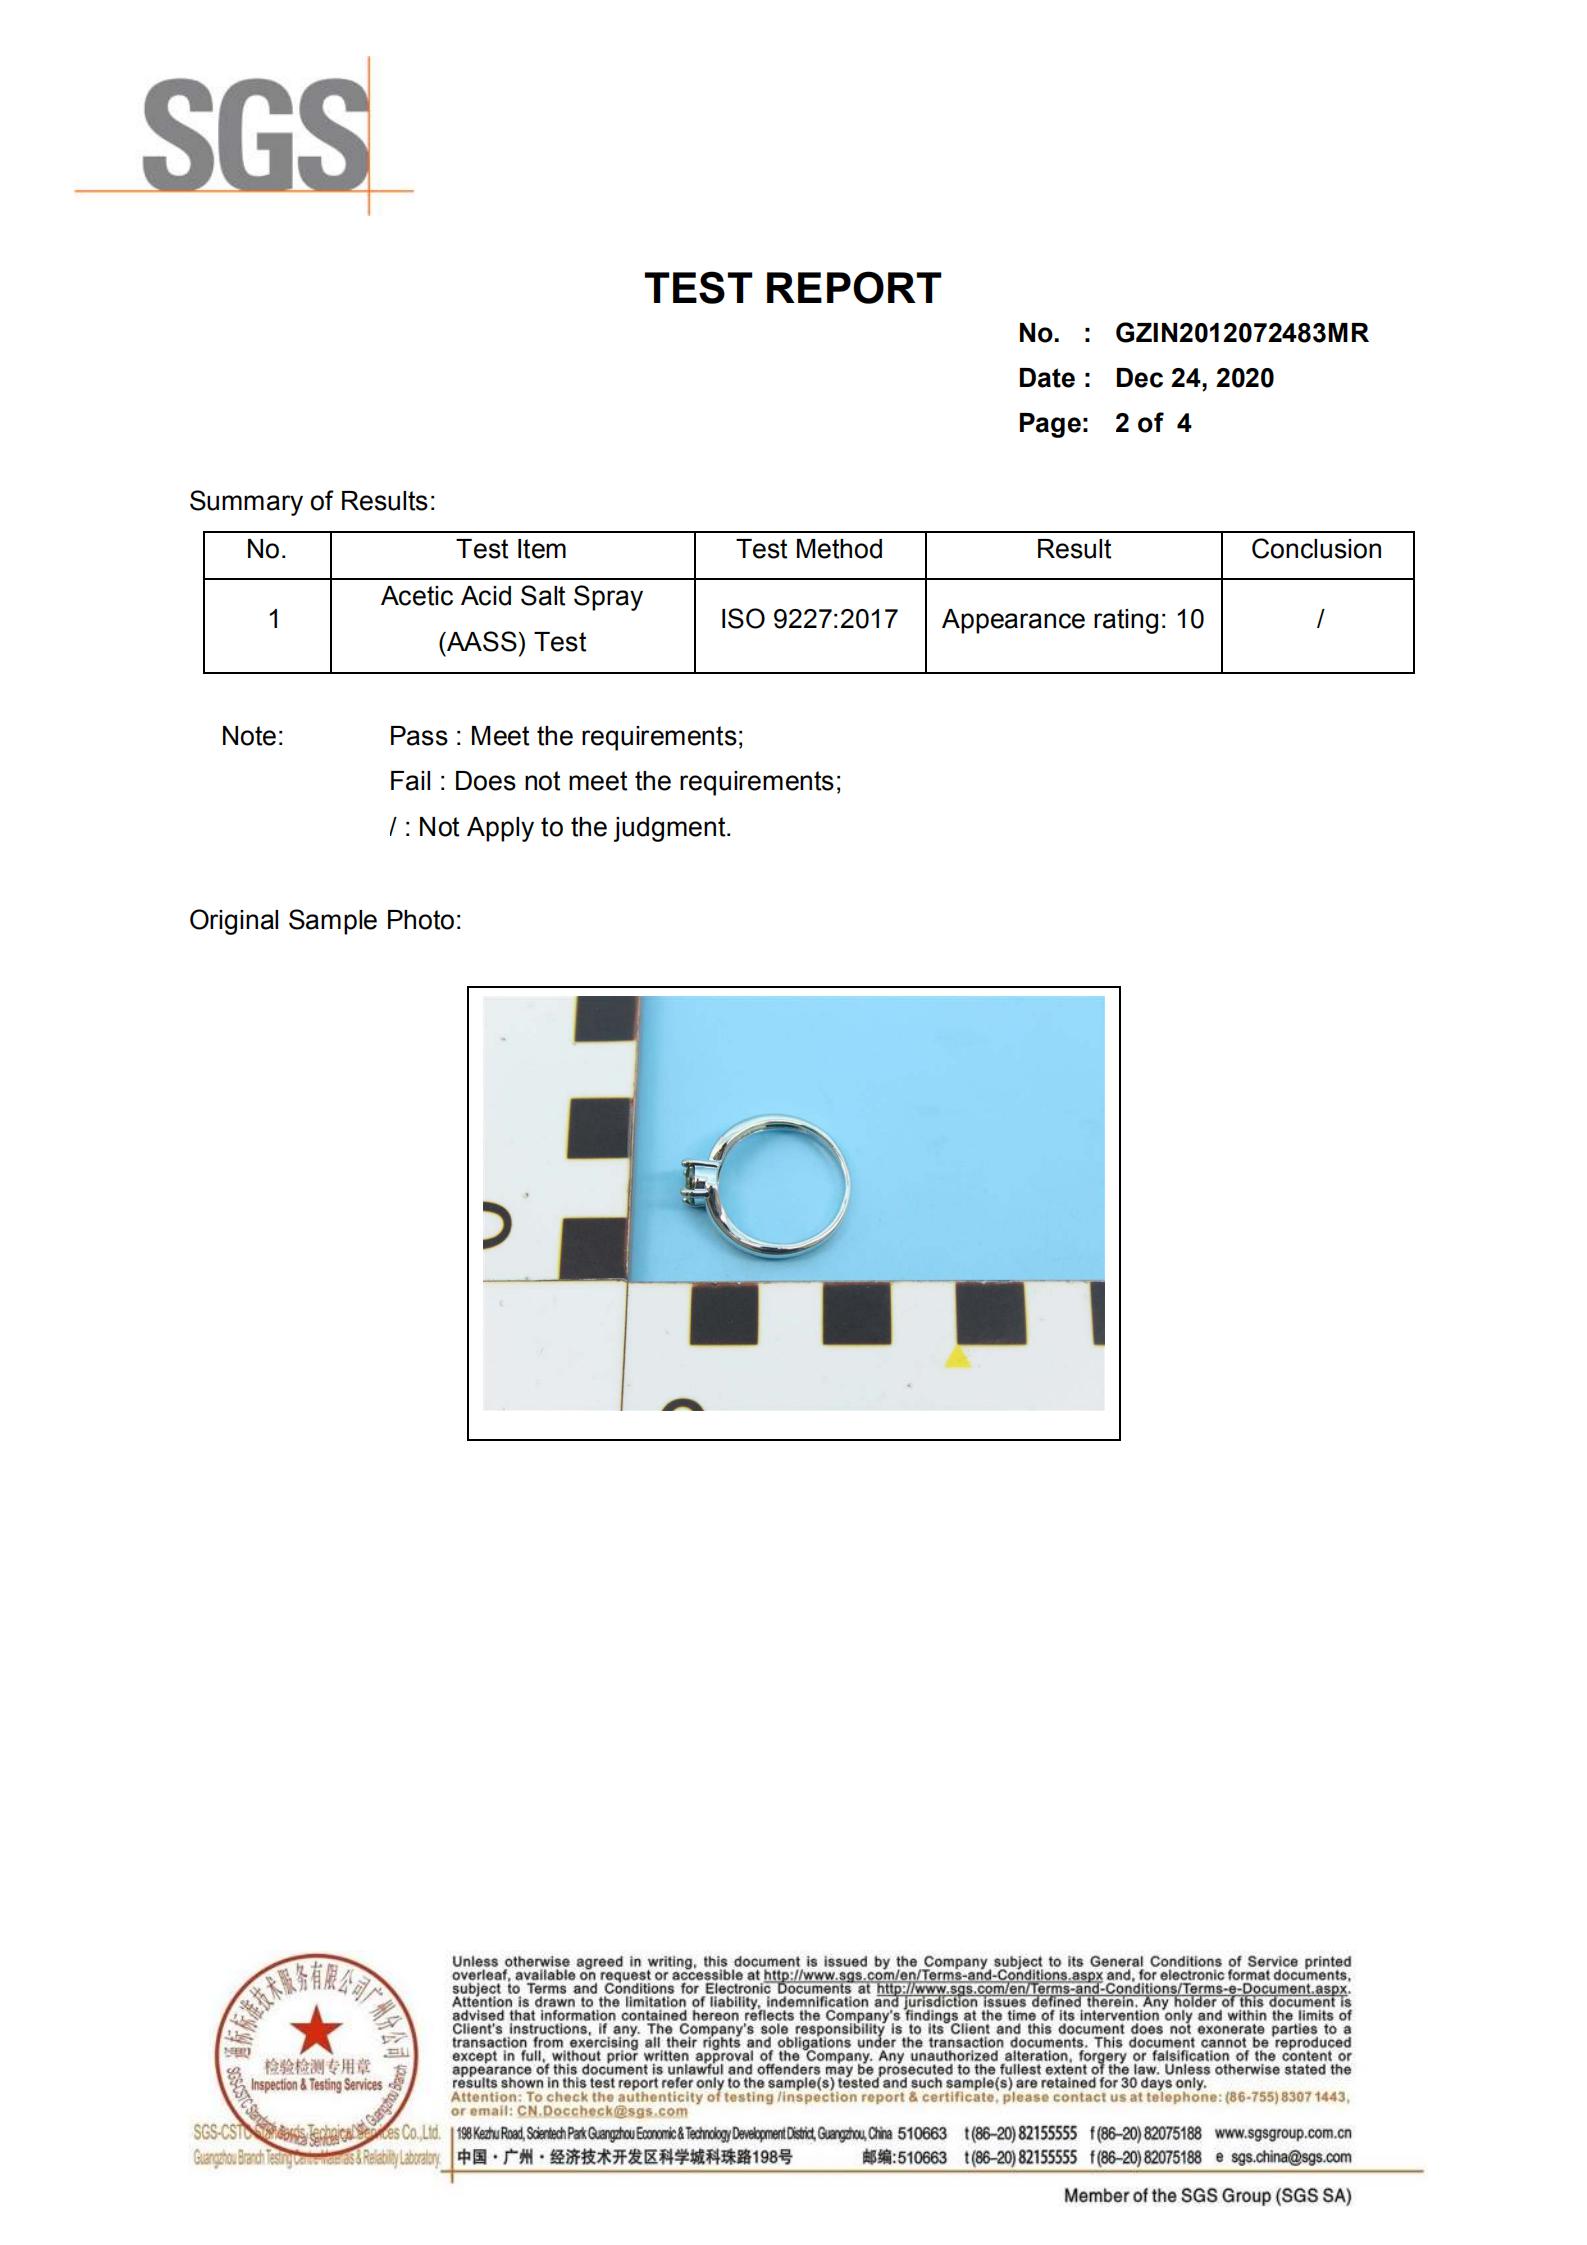
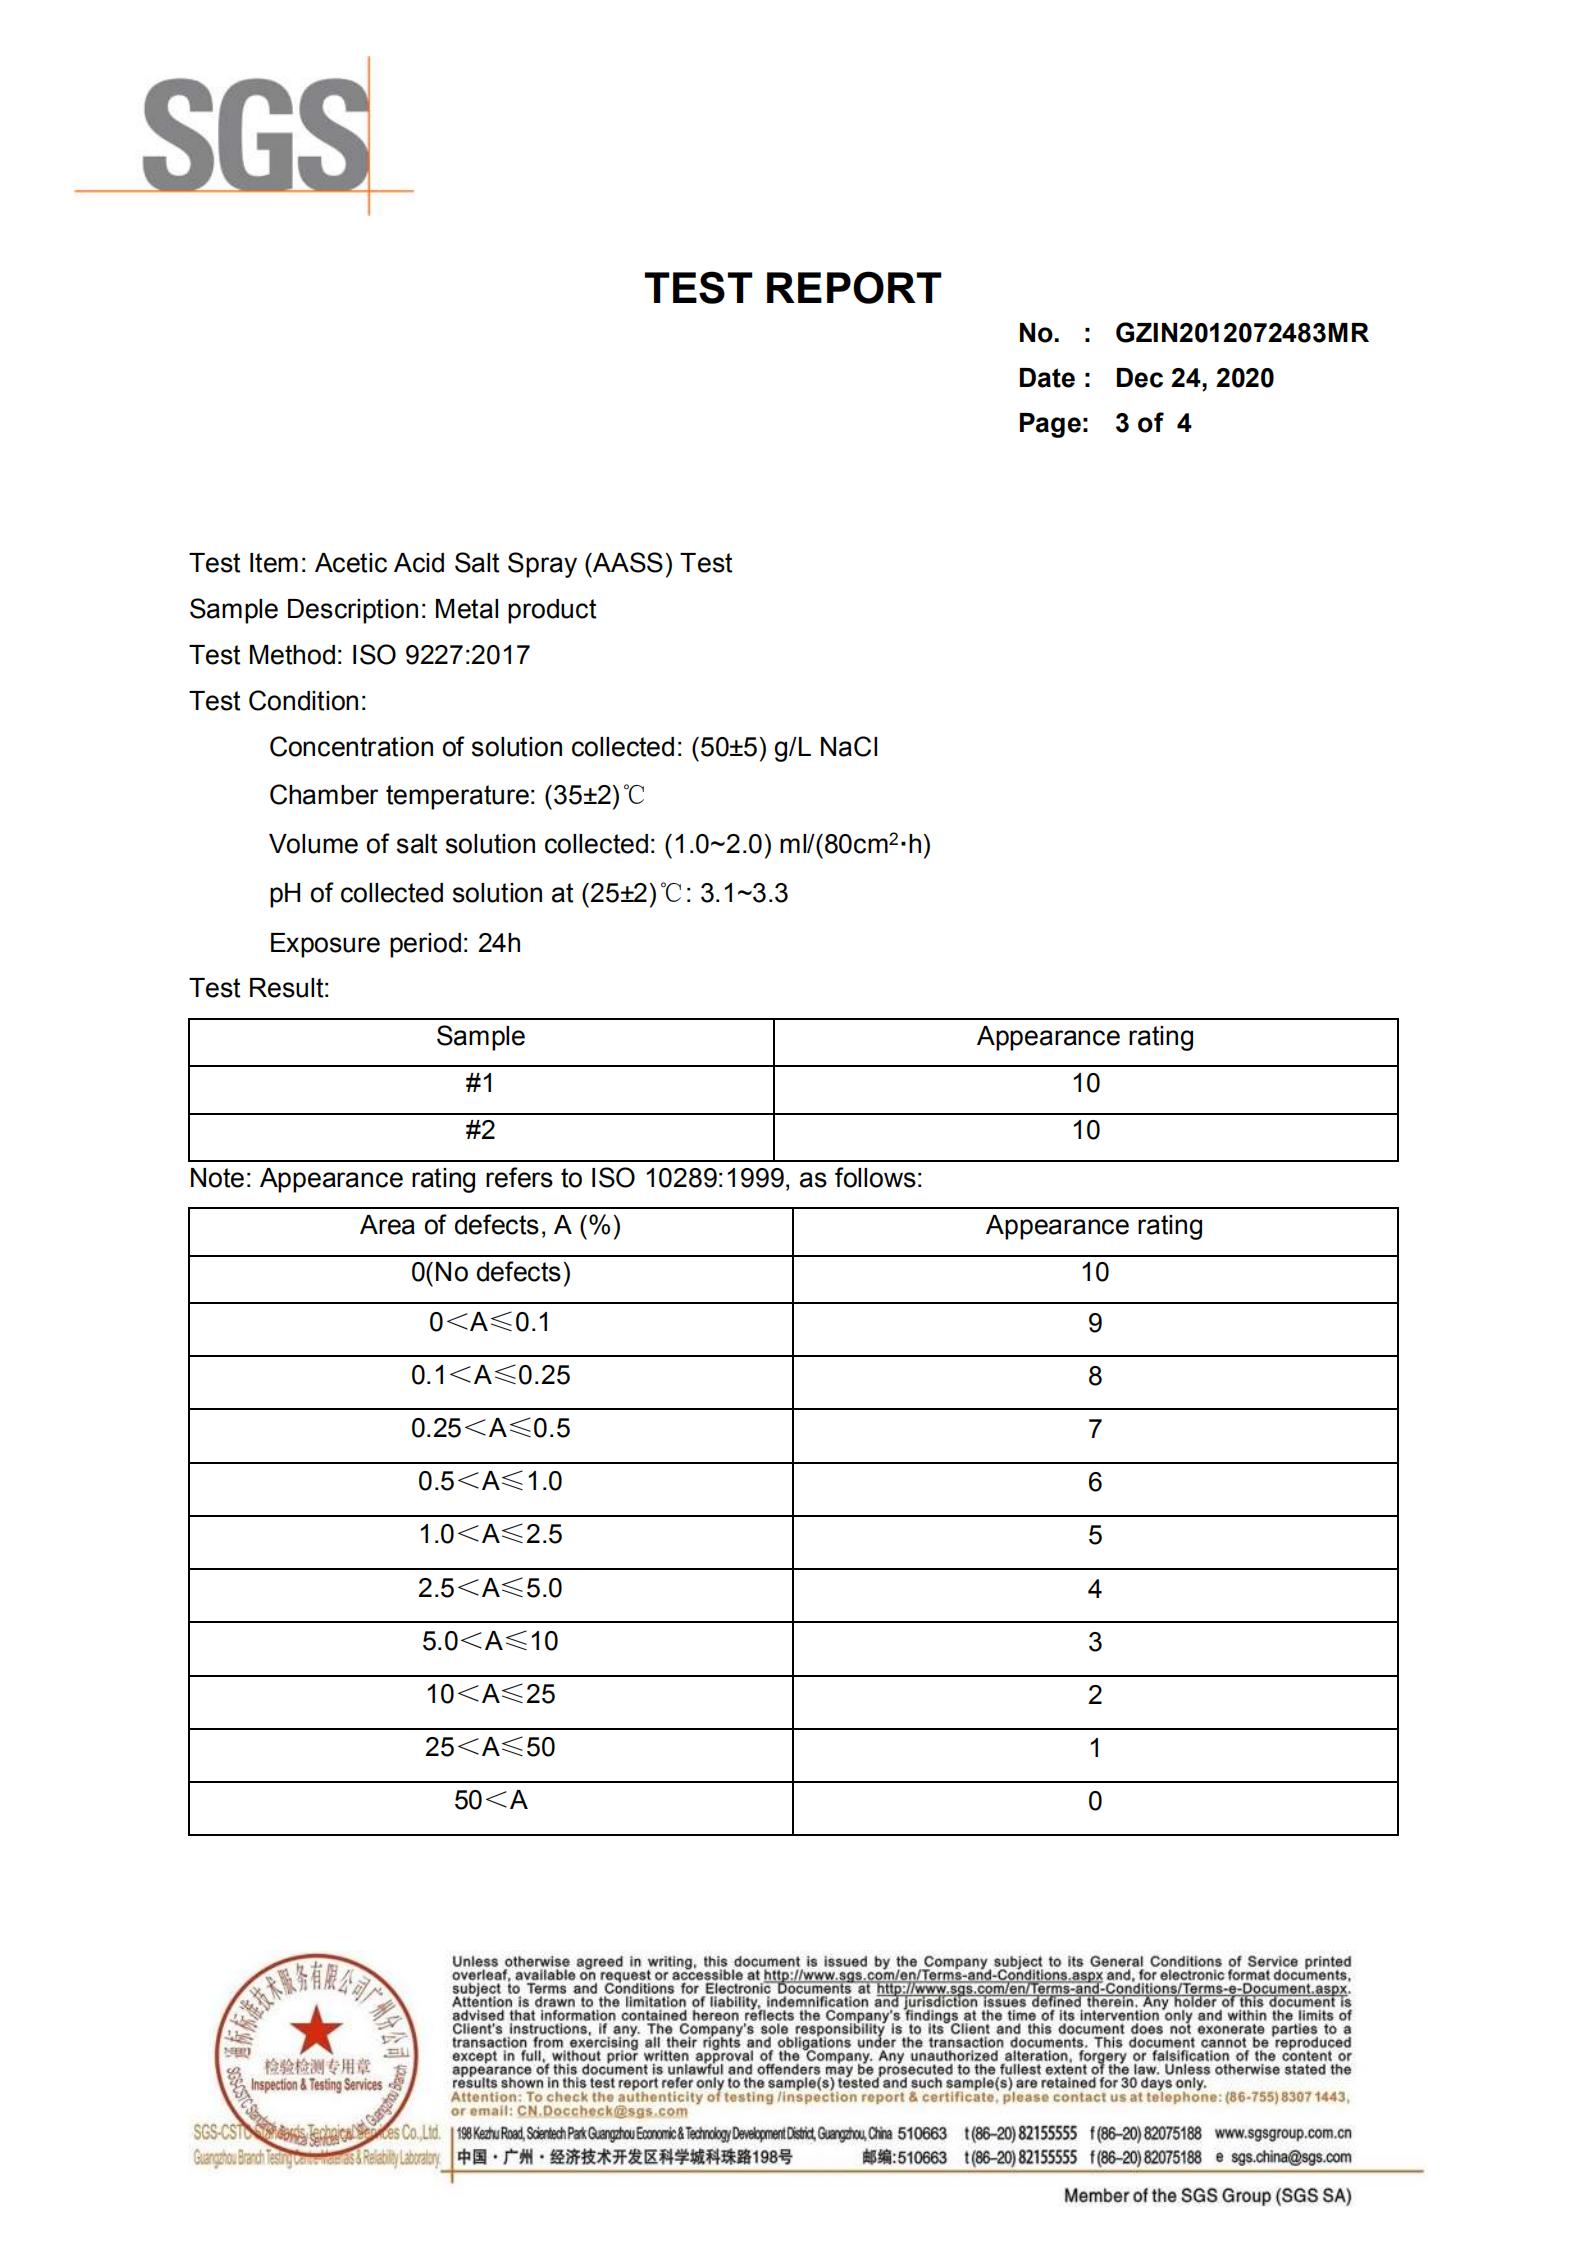
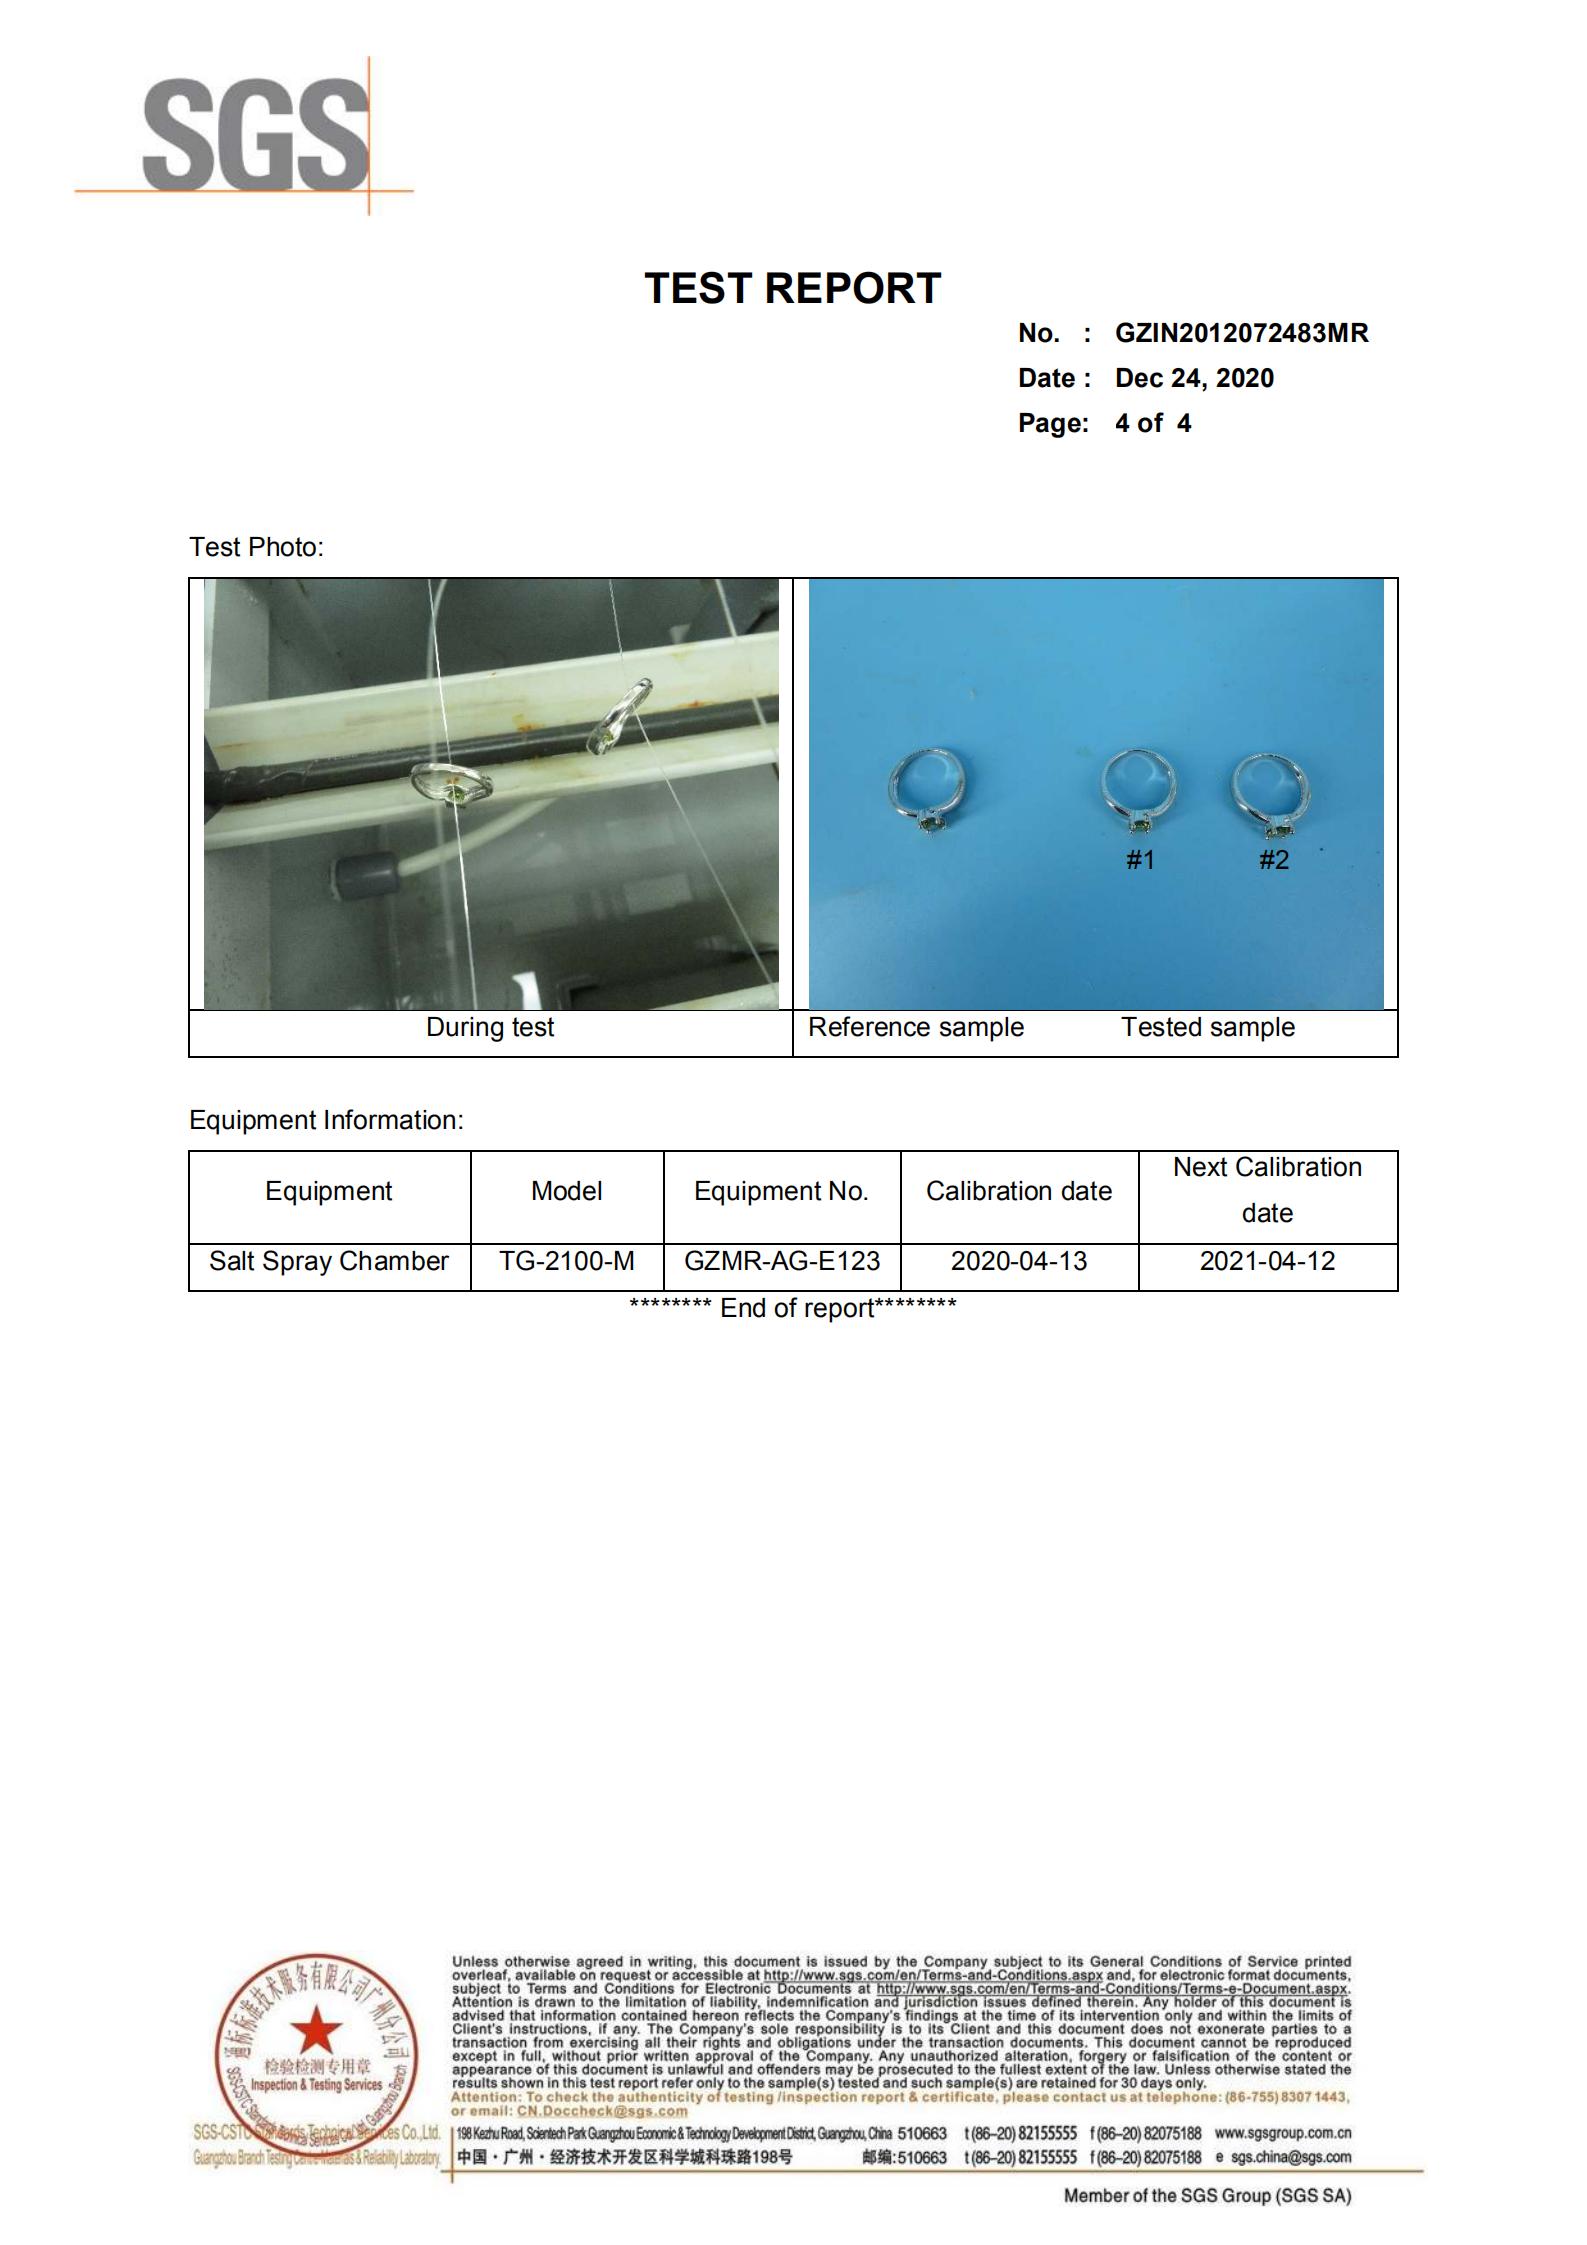
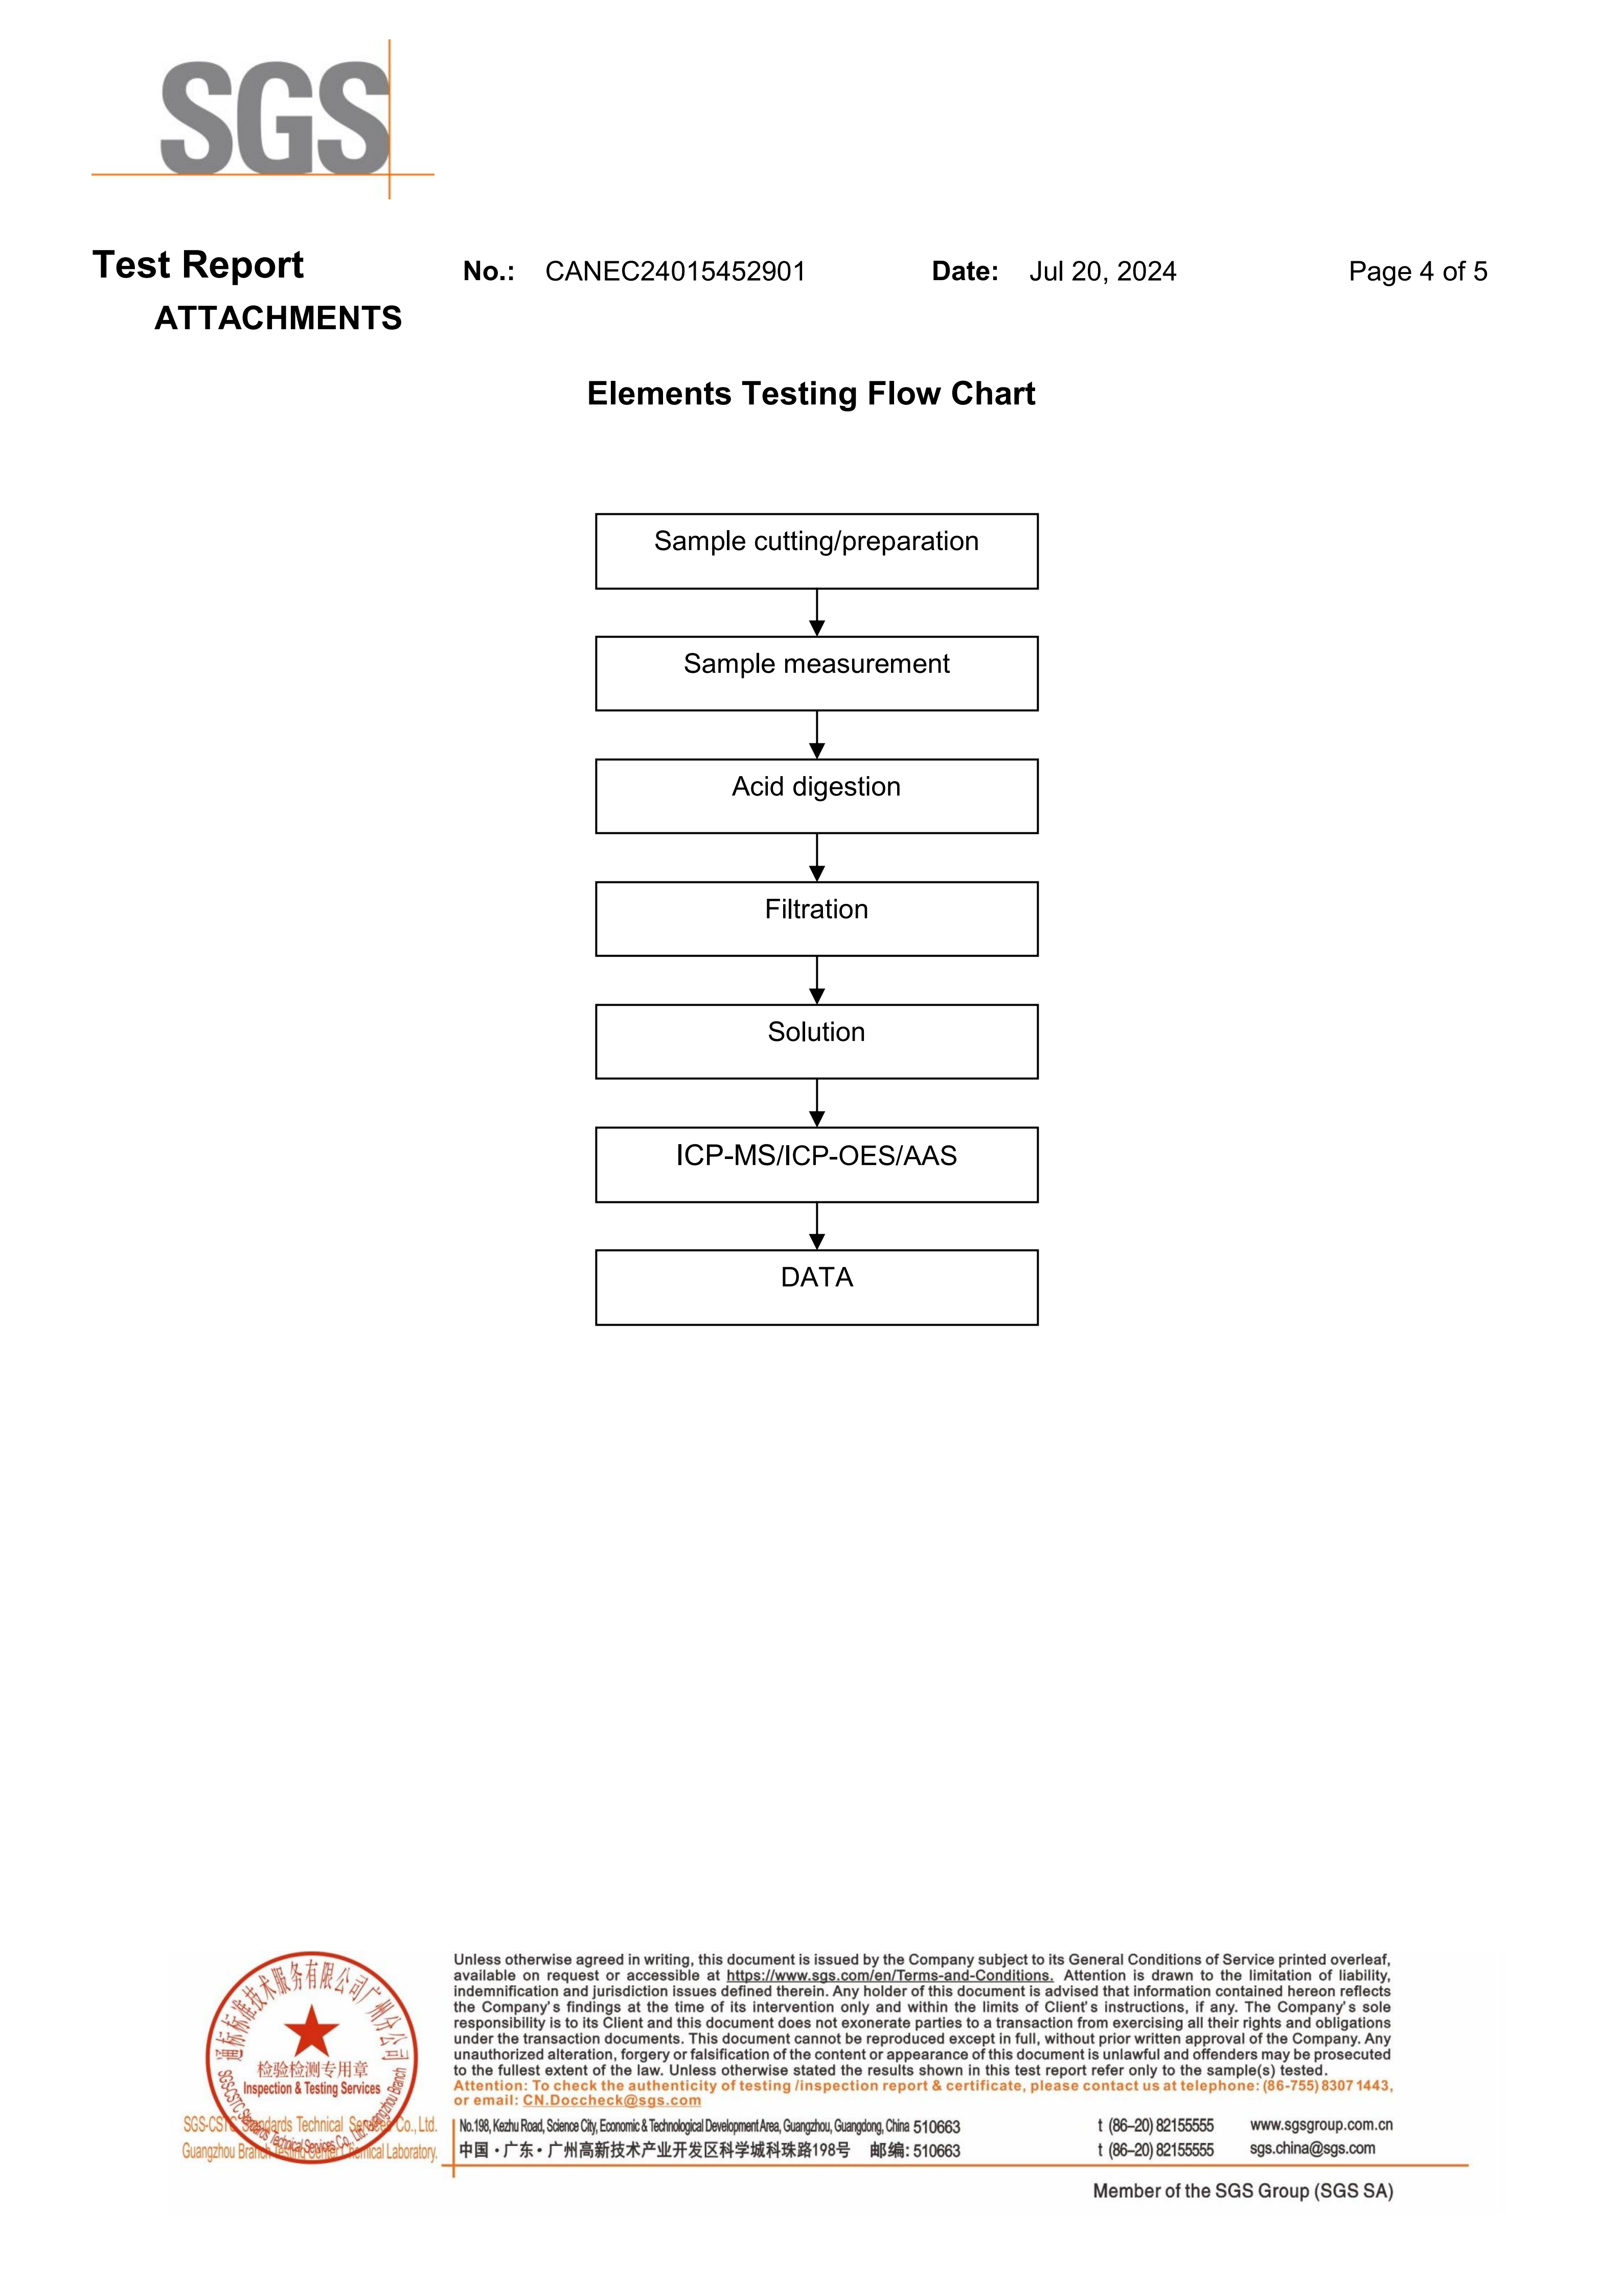
ISO 9227:2022, Corrosion Tests in Artificial Atmospheres—Salt Spray Tests, specifies neutral salt spray, acetic acid salt spray, and copper-accelerated acetic acid salt spray procedures. The ISO page identifies these methods as NSS, AASS, and CASS, respectively.
Salt-spray testing can reveal pores, discontinuities, physical damage, and other coating weaknesses that allow corrosive agents to reach the underlying metal. However, it is a controlled comparative test rather than a direct prediction of real-life service life.
Passing a specified number of salt-spray hours does not prove that a jewelry product will retain its color for an equivalent number of months or years. The buyer and manufacturer must agree on the exact test method, duration, sample preparation, evaluation area, and permitted level of discoloration or corrosion.
ISO 9227:2022 currently has one published amendment:
How Buyers Should Interpret Test Results
Laboratory testing provides controlled comparative evidence, but no single result can reproduce every real-life wearing condition.
An XRF reading at one location does not prove identical thickness across an entire ring, chain, or textured pendant. Artificial-sweat testing does not represent every consumer’s sweat chemistry. Salt-spray testing does not reproduce normal jewelry care, and abrasion testing may not reflect the deformation experienced by an adjustable design.
Buyers should therefore evaluate the complete validation package rather than relying on one report or one headline number. A reliable approval package normally combines material confirmation, an approved physical color sample, a documented coating structure, thickness measurements at agreed locations, relevant adhesion or corrosion results, and a bulk inspection plan.
Test reports should also match the production construction. A report for one base alloy, soldering process, or coating structure should not automatically be used to support a materially different product.
Cost, MOQ, and Lead-Time Considerations
Neither PVD nor electroplating is universally cheaper.
PVD quotations are influenced by the coating chemistry, chamber setup, fixture design, number of product orientations, loading efficiency, pretreatment requirements, and production quantity. A small order requiring a unique color or dedicated fixture may carry a relatively high setup cost per piece.
Electroplating costs are strongly affected by precious-metal prices, required karat, coating thickness, surface area, intermediate layers, polishing, bath control, inspection, and rework. A thicker genuine-gold layer will normally cost more than a very thin decorative finish because it uses more precious metal.
A hybrid electroplating-and-PVD system usually involves additional steps and should not automatically be presented as the lowest-cost solution. Its added complexity should support a defined requirement such as improved leveling, better barrier protection, an engineered color, or a specific wear-performance target.
Lead time is also affected by color development, sample revisions, fixture preparation, stone-setting sequence, laboratory testing, and production quantity. Buyers should therefore compare quotations based on an agreed specification rather than comparing unit prices for products described only as “PVD” or “gold plated.”
From Quotation to Bulk Production
An accurate coating quotation begins with complete product information. The buyer should provide clear product images or CAD files; base material; dimensions; surface finish; target color; destination market; estimated quantity; and any genuine gold, thickness, or compliance requirements. Stone types, adhesives, and moving components should also be disclosed because they may affect the production sequence.
In response, the manufacturer should explain the proposed layer structure, confirm whether the visible finish contains genuine gold, identify the measurement and testing methods, and highlight any design risks. The sample stage should establish the approved color, gloss, texture, coating structure, and required test results.
A physical master sample is generally more reliable than a photograph for final color approval because lighting, camera settings, and screen displays can significantly alter the appearance of gold and other decorative finishes.
Once the sample is approved, the same information should be transferred into the bulk-production specification. This document should identify the approved sample, base material, coating structure, target thickness, accepted tolerance, inspection frequency, and procedure for handling failed results.
How to Evaluate a PVD or Electroplating Manufacturer
A qualified jewelry manufacturer should evaluate more than the requested surface color. The supplier should review the base material, product geometry, soldering, polishing, stones, flexibility, and intended product claims before recommending a coating system.
Professional buyers should expect the manufacturer to explain the complete layer structure, confirm precious-metal content where applicable, define XRF measurement locations, and provide an appropriate sample and testing plan.
Warning signs include using “PVD gold,” “18K color," and “18K gold plated” as interchangeable terms; promising permanent waterproofing without test conditions; quoting a thickness without identifying the measured layer; or using one test report to support products with materially different constructions.
A strong supplier should also be willing to discuss realistic limitations. Technical caution is generally more credible than an unconditional promise that every material, design, and coating will perform in the same way.
Final B2B Recommendation
Choose PVD coating when the collection requires an engineered decorative color, a hard visible surface, and improved abrasion performance on a compatible, properly prepared product.
Choose traditional electroplating when the product requires genuine precious-metal content, a specified karat and thickness, surface leveling, diffusion barriers, or broader coverage across complex conductive geometry.
Consider an electroplating-and-PVD system when electroplated layers are needed to create a smooth and corrosion-resistant foundation and a PVD film is required for the final color or wear characteristics.
For 925 sterling silver and premium brass jewelry, the final decision should be based on a design review and validated sample. The base alloy, soldering, stone setting, product flexibility, destination market, and intended marketing claims can all affect the correct coating structure.
Request a Design-Specific Coating Recommendation
Zhefan Jewelry supports OEM and ODM development for 925 sterling silver and premium brass jewelry, including traditional electroplating, PVD coating development, gold vermeil production, multilayer finishing, coating-thickness inspection, and compliance testing support.
Our team can review the design and prepare a proposed coating structure, sample-validation plan, and production quotation before bulk manufacturing.
FAQ
Is PVD better than electroplating for jewelry?
Not universally. PVD may provide a harder engineered surface, while electroplating is more suitable for genuine precious-metal layers, surface leveling, barrier layers, and many complex shapes. The correct process depends on the complete product specification.
Does gold-colored PVD contain real gold?
Not always. Many gold-colored PVD coatings use titanium- or zirconium-based compounds. Buyers should confirm the deposited material and full coating structure before making gold-content claims.
Can brass jewelry be PVD coated?
Yes, selected brass jewelry can be PVD coated. Surface preparation and electroplated intermediate layers may be required to improve leveling, adhesion, and barrier performance.
Can 925 sterling silver jewelry be PVD coated?
Yes, for suitable designs. The manufacturer should review the silver alloy, soldering, polishing, stones, flexibility, and process compatibility before confirming production.
Does PVD last longer than gold plating?
A hard PVD film may resist abrasion better than a very thin decorative gold layer. Actual service life still depends on substrate preparation, adhesion, porosity, underlayers, product structure, and wearing conditions.
Is PVD jewelry waterproof?
PVD can improve resistance to moisture and corrosion, but it should not automatically be marketed as permanently waterproof. Any water-resistance claim should be supported by a defined test and realistic usage conditions.
Can PVD replace gold vermeil?
A non-gold PVD coating cannot replace the genuine gold or gold-alloy covering required for a vermeil claim. Compliance depends on the sterling silver base, gold fineness, equivalent fine-gold thickness, significant surface coverage, and any required disclosures.
Is PVD automatically nickel-free or hypoallergenic?
No. The complete product—including the base metal, solder, intermediate layers, final coating, and exposed areas—must be evaluated.
Can PVD be applied after stone setting?
Sometimes. Compatibility depends on the stone, treatment, adhesive, setting method, vacuum environment, and process temperature. The production sequence should be established through sample testing.
Which tests should jewelry buyers request?
The appropriate test plan depends on the product and destination market. It may include coating-thickness measurement, adhesion, salt spray, artificial sweat, abrasion, flex testing, nickel release, and restricted-substance testing.
Does passing a salt-spray test prove years of color retention?
No. Salt-spray testing is useful for comparative corrosion evaluation and identifying coating weaknesses, but the test duration cannot be converted directly into months or years of consumer wear.
What information should be included in a coating quotation request?
The buyer should provide the base material, design files, dimensions, surface finish, target color, genuine gold requirements, order quantity, destination market, stone information, and required tests.
Recommended for you

What Is Gold Vermeil Jewelry? A Complete Guide for Brands and Retailers

Thick Gold Plated Jewelry Manufacturer for 925 Silver & Brass Jewelry

How to Choose a Gold Vermeil Jewelry Manufacturer

Can Silver or Brass Be PVD Coated? A Professional Guide for Jewelry Brands
Product Categories
Discuss Your Ideas with a Professional Custom Jewelry Manufacturer
We provide personalized jewelry customization services for clients worldwide.
Rest assured that your privacy is important to us, and all information provided will be handled with the utmost confidentiality.
By clicking 'Send Inquiry Now' I agree to ZHEFAN JEWELRY processing my personal data.
To see how to withdraw your consent, how to control your personal data and how we process it, please see our Privacy Policy and Terms of use.
From design to production, ZHEFAN JEWELRY offers a one-stop solution to help you enhance your brand value and market competitiveness.
Get A Quote
Contact
Tel: (+86) 188 1927 7817
© 2026 Zhefan Jewelry. All Rights Reserved.
Facebook
Instagram
YouTube
Whatsapp: +8618819277817